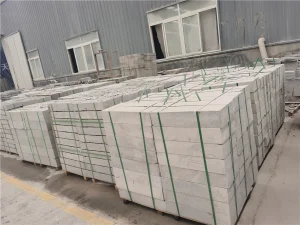
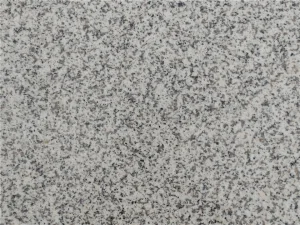
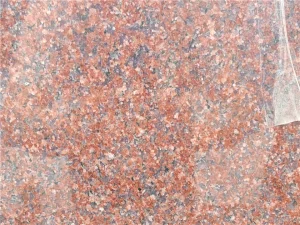
Standard & Custom Sawn Slab Showcase (Batch I)
Explore our core natural stone inventory engineered for high-load architectural applications, monolithic table tops, and integrated interior structural furniture.
Engineering Travertine Stone Tables: Precision Craft Meets Sedimentary Mineralogy
The global shift toward biophilic architectural spaces, warm minimalism, and monumental organic stone furniture has established travertine as the definitive luxury medium of 21st-century interior design. Unlike dense igneous plutonic rock (such as granite) or metamorphosed calcite (marble), travertine is a terrestrial sedimentary limestone deposited by mineral springs, characterized by cellular voids, fibrous calcitic banding, and rhythmic thermal layering. Engineering functional, deflection-resistant travertine dining tables, monolithic plinths, and fluted coffee tables requires a multi-tiered synthesis of raw block geological evaluation, structural void stabilisation, multi-axis 3D CNC contouring, and advanced pore-filling technology.
Geological Matrix Integrity
Assessing travertine lithotypes (Navona White, Classic Roman Beige, Iranian Silver, Tuscan Walnut) based on bulk specific gravity (2.30 to 2.52 g/cm³) and structural porosity. Our block selection process eliminates deep micro-fissuring before secondary diamond gang-sawing.
Sub-Surface Vacuum Consolidation
Treating raw slabs with advanced thermoset vacuum-infused polyester and breathable elastomeric resins. By calibrating UV-stable mineral colorants, natural cavernous voids are hermetically sealed or selectively preserved to achieve the requested tactile patina.
Sub-Millimeter Structural Tolerance
Large dining tables (2.4m to 3.6m cantilevered spans) undergo finite element modeling (FEM) to balance dead-weight deflection. Carbon-fiber stiffener rods and aviation honeycomb backings are integrated to mitigate shear stresses while retaining natural stone aesthetics.
China Factory 4.0: Supply Chain Resilience, Scalability & Sub-Millimeter Fabrication
How our vertically integrated Rizhao production ecosystem merges deep mineral extraction with automated digital manufacturing to eliminate cost overruns, delivery delays, and dimensional variances.
Automated Multi-Axis CNC & Waterjet Routing
Travertine tables often demand intricate architectural bases: Roman columns, organic egg profiles, fluted monoliths, and sculpted sphere supports. Our workshop leverages Breton and CMS 5-axis interpolated CNC milling heads coupled with 60,000 PSI ultra-high-pressure abrasive waterjets. This ensures complex geometries match 3D CAD/CAM models with tolerances under ±0.5mm, enabling seamless lock-and-key internal joinery without visible mechanical anchoring.
Deep Port-Side Industrial Clustering
Situated within the Shandong Stone Cluster directly linked to Rizhao Port and Qingdao Hub, our facility provides streamlined logistics that cut transit costs by up to 30%. Raw Italian, Turkish, Iranian, and Chinese travertine blocks arrive directly via sea container, are processed under automated continuous diamond lines, and are packaged for export without intermediary haulage delays. This enables rapid delivery schedules for hotel rollouts and multi-unit residential contracts.
Full-Spectrum Vein Orientation: Vein-Cut vs. Cross-Cut
The mechanical strength and aesthetic rhythm of a travertine table are fundamentally dictated by the sawing axis. We offer both Vein-Cut (transverse across the bedding planes, revealing parallel linear striations reminiscent of geological strata) and Cross-Cut (fleuri-cut parallel to the bedding plane, producing open cloud-like tonal swirls). Our optical sorting algorithms ensure vein continuity wraps across mitered waterfall table edges with mathematical continuity.
Technical Roadmap: Structural Engineering, Anti-Etch Hydrophobicity & Lightweighting
Natural travertine presents distinct mechanical challenges: porous surface vulnerabilities, susceptibility to acidic etching (citric juice, wine, coffee), and substantial self-weight (approx. 70 kg per m² at 30mm solid thickness). As a Tier-1 manufacturer, we have developed advanced material handling systems that elevate stone table reliability beyond traditional workshop limitations.
| Evaluation Parameter | Standard Commercial Travertine | Factory 4.0 Engineered Travertine Table | Testing & Compliance Reference |
|---|---|---|---|
| Pore Treatment Finish | Open porous or coarse mastic filler | Nano-calcite vacuum impregnation / Food-grade epoxy | ASTM C170 / EN 1936 Porosity Standard |
| Surface Stain Resistance | Stains readily (pH < 6 reacts in 5 min) | Fluoro-silane hydrophobic shield (48 hr acid barrier) | ISO 10545-14 Chemical Resistance Class A |
| Flexural Strength (Modulus) | 4.5 - 6.2 MPa (inherent bedding plane weakness) | 14.8 - 19.5 MPa (carbon-fiber rod + mesh reinforcement) | ASTM C880 / EN 12372 Flexural Verification |
| Table Top Dead-Weight | 100% Solid Mass (~72 kg/m² @ 30mm) | Ultra-light composite (~26 kg/m² with honeycomb core) | Aviation Structural Honeycomb ISO 9001 |
| Miter Joint Structural Bond | Manual knife-grade polyester paste | Automated CNC beveling + structural methacrylate glue | EN 14617-2 Internal Bonding Cohesion |
Tri-Stage Anti-Stain Nano Sealing
Untreated travertine absorbs moisture at rates between 1.5% and 3.0%. For dining and conference table configurations, we apply a deep-penetrating fluoro-silane polymer treatment that chemically cross-links with the calcitic crystalline matrix. This maintains an oleophobic and hydrophobic barrier without forming an artificial plastic shine, preserving the honed satin feel while passing stringent hotel staining tests.
Aviation Honeycomb Composite Engineering
For large-scale executive conference tables spanning up to 4.5 meters, solid monolithic stone becomes prohibitive due to elevator transport limits and subfloor load limits. Our lightweight engineering bonds a 5mm to 8mm calibrated travertine veneer to an aerospace-grade aluminum honeycomb substrate, decreasing weight by over 60% while multiplying tensile flexural resistance threefold.
Interlocking Metal-to-Stone Chassis Systems
Traditional stone tables rely on dangerous gravity-only placement or messy site gluing. We engineer integrated CNC stainless steel insert bushings (SUS304/SUS316) into the stone underbelly. This allows demountable, rigid bolt fastening to custom steel, brass, bronze, or stone base structures, ensuring absolute seismic stability and zero lateral sway during contract installation.
Macro Industry Solutions: Tailored Furniture Systems for Global Commercial Sectors
From high-turnover luxury hospitality dining spaces to bespoke architectural residences, we supply pre-engineered, modular, and monolithic natural stone table solutions built to withstand heavy daily use.
Luxury Hospitality (Hotels & Resorts)
Providing heavy-duty travertine banquet tables, outdoor terrace bistro tables with freeze-thaw protection, hotel lobby focal plinths, and guestroom console desks. We offer batch consistency across hundreds of units with pre-installed leveling glides and anti-tip base weights.
Bespoke Residential & Villa Developments
Partnering with world-class interior designers to execute one-of-a-kind organic sculptural dining centerpieces, live-edge hollowed travertine blocks, waterfall kitchen islands, and book-matched fluted coffee tables crafted to bespoke shop drawings.
Corporate Headquarters & Boardrooms
Engineering monolithic conference tables equipped with flush-mounted wireless charging stations, hidden cable management raceways, and concealed pop-up audiovisual panels routed into the travertine surface via high-precision CNC dry milling.
Luxury Flagship Boutiques & Retail
Creating branded display plinths, tiered jewelry display tables, cash wraps, and sculptural seating blocks. Our multi-material capabilities merge travertine with brushed brass, smoked glass, and PVD titanium coated stainless steel framework.
Global Enterprise Sourcing: Quality Control, Tolerance Matrices & Export Protocols
Purchasing natural stone furniture across international borders requires stringent risk mitigation. We remove uncertainty for general contractors, specifiers, and procurement agencies through a systematic 6-tier quality verification process.
Full Dry-Lay Vein & Shade Harmonization
Before final packing, every table top and base component is assembled in our 4,800 m² dry-lay hall. Slabs are photographed under standardized 6500K color-balanced illumination. Clients receive high-resolution photo and 4K video documentation for vein confirmation, edge miter alignment, and tone consistency approval.
Reinforced Sea-Freight Packaging Engineering
Natural stone furniture failures occur when crating is treated as an afterthought. We construct ISPM-15 fumigated solid pine export crates braced with customized high-density EVA shock-absorbing foam molds, corner edge guards, and vapor-barrier desiccant bags to prevent moisture entrapment during tropical sea routes.
Complete Commercial Contract Compliance
We provide full documentation for international project customs clearance: Certificates of Origin (CO, Form E, Form F), commercial invoices, itemized packing lists with piece-number shop drawings, ASTM C615 / C170 physical testing reports, and VOC-free sealant emission certifications.
Localized Support & International Standards Compliance
Ensuring frictionless site delivery, structural safety adherence, and multi-regional regulatory conformance across North America, Europe, Australia, and the Middle East.
Dedicated Project Timezone Desk
Our dedicated project engineering teams operate across overlapping timezones with Europe (CET), North America (EST/PST), and the Gulf (GST). Detailed CAD shop drawing revisions and structural adjustments are turned around in 24 hours.
International Safety Certification
All structural adhesives and honeycombs comply with UL 94 V-0 flame-retardant requirements. Surface sealants conform with European REACH regulations and US FDA/NSF non-toxicity standards for safe food contact in hospitality dining rooms.
On-Site Installation Coordination
Each table arrives with an indexed assembly guide, numbered components, precision brass shims, and pre-fitted lifting strap positions. We offer remote video supervision and dispatch master stonemasons for large-scale international commercial projects.
Frequently Asked Questions: Sourcing Travertine Stone Tables from China
Expert answers addressing structural viability, resin selection, maintenance protocols, and international B2B logistics.
What is the structural difference between "Filled" and "Unfilled" travertine tables?
Unfilled travertine preserves the organic cellular cavities created by geothermal gas escapes during mineral formation, delivering an earthy, tactile, wabi-sabi aesthetic. However, for commercial dining use, filled travertine is strongly recommended. We fill voids using color-matched calcitic cement or transparent, UV-stable Italian polyester epoxy, creating a smooth, hygienic surface that stops food particles, sauces, and liquids from penetrating the stone matrix.
How do you prevent large cantilevered travertine tables from cracking along the vein?
Because travertine exhibits natural sedimentary bedding planes (especially in vein-cut formats), its tensile strength along bedding lines is lower than granite. For spans exceeding 1.8 meters, our engineers mill blind structural slots into the slab underside and embed twin pultruded carbon-fiber reinforcement rods bonded with structural structural epoxy. For ultra-thin profiles, we bond the slab directly to an aviation-grade aluminum honeycomb backing plate.
Can travertine tables be utilized in exterior restaurant patios and garden environments?
Yes, provided appropriate block grading and weatherproofing treatments are applied. Exterior travertine must feature open-pore or frost-resistant breathable cementitious filling rather than standard indoor epoxies, which degrade under sun exposure. Slabs receive a sub-surface hydrophobic seal that allows moisture vapor to breathe out while preventing water pooling, protecting against freeze-thaw spalling in temperate climates.
What finishes are available, and which is optimal for luxury furniture?
We provide Honed (matte 15-25% sheen, velvety tactile texture, optimal for luxury residential), Polished (mirror reflectivity, highlighting crystal depth), Brushed/Leathered (textured via diamond wire brushes for an antique patinated finish), and Bush-hammered (heavily textured for architectural monolithic pedestals). Honed with micro-chamfered edges remains the benchmark specification among leading international design firms.
How is vein-matching maintained across multi-piece conference tables?
All components for multi-piece tables are cut sequentially from the same monolithic travertine block using synchronized 5-axis saw blades. Slabs undergo computerized scanning where our CAD nesting software calculates cut paths down to the millimeter. This guarantees that horizontal flowing strata transition effortlessly across table seams, drop waterfall edges, and down vertical monolithic base plinths.
What are your standard export lead times and minimum order quantities (MOQ)?
Our standard MOQ is flexible for project contracts—ranging from single bespoke signature boardroom tables to complete hotel programs of 200+ tables. Sample production and shop drawings require 5 to 7 days, full production takes 3 to 4 weeks depending on batch volume, and container stuffing is coordinated directly from Rizhao or Qingdao port for efficient sea-freight dispatch worldwide.
Architectural Granite, Limestone & Cladding Selection (Batch II)
Explore our secondary natural stone material inventory engineered for heavy municipal pavements, exterior facades, integrated curbstones, and monolithic plinths.