
Engineered Facade Veneers & Natural Stone Ensembles
Explore our premium architectural panels and quarry-calibrated structural units manufactured under rigorous ISO/CE quality systems for global commercial installations.
Engineering Paradigms of Artificial Stacked Stone
Addressing structural load limitations, environmental degradation, and thermal performance through next-generation cultured stone compositions and automated fabrication lines.
Material Science & Aggregate Chemistry
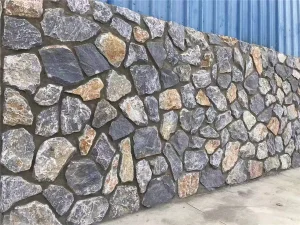
Modern artificial stacked stone (also classified as manufactured stone veneer, architectural ledger stone, or cultured stone) has evolved far beyond basic precast concrete. Today's industrial production leverages high-grade Portland cement, expanded shale, lightweight cellular aggregates, pozzolanic micro-silica, and inorganic UV-resistant Bayer iron oxide pigments. This synthetic composition yields compressive strengths surpassing 25 MPa while mitigating excess dead load by 60% compared to quarried rubblestone.
Precision Moulding & Morphological Fidelity
By capturing hyper-detailed silicone and polyurethane impressions directly from authentic fractured slate, dry-stacked quartzite, and rough-faced granite boulders, precision casting lines achieve zero repetitive tiling patterns over 50 square meters. The interlocking tongue-and-groove engineering minimizes thermal bridging, conceals mortar seams, and expedites rapid site installation across residential and commercial substructures.
Severe Climate Durability Dynamics
Equipped with reactive silane-siloxane impregnations, engineered artificial stone matrices demonstrate water absorption coefficients below 6% (conforming to ASTM C1670 standards). This ultra-dense cellular integrity precludes moisture ingress, completely eliminating spalling, efflorescence migration, and freeze-thaw micro-fissuring across extreme sub-zero exterior envelopes (-40°C to +80°C operating thresholds).
China's Manufacturing Hub: The Supply Chain Ecosystem
Why Tier-1 architectural developers and tier-one construction material wholesalers consolidate their procurement directly within China's specialized coastal manufacturing clusters.
Vertically Integrated Raw Minerals
Situated in prominent stone-processing regions such as Rizhao, Shandong, factories enjoy unhindered access to hyper-pure volcanic pozzolana, natural aggregates, and high-strength white cement reserves. This immediate regional raw material availability stabilizes unit pricing against international inflationary shifts.
Automated Continuous Curing Lines
Advanced Chinese facilities utilize constant-temperature steam hydration chambers and computer-controlled dosing stations. This industrial-scale automation shortens post-moulding curing cycles from 28 standard days to 72 hours without inducing micro-shrinkage tension or compromise to final compressive modulus.
Deep-Water Port Intermodal Efficiency
Operating within brief trucking radii of Rizhao Port and Qingdao Port, manufacturing hubs eliminate inland freight demurrage. Project consignments transition seamlessly from multi-axis crate-palletizing lines directly into ocean container berths, maintaining consistent transpacific and transatlantic schedules.
Comprehensive OEM/ODM Capabilities
Global brands collaborate directly with in-house CAD tooling engineers to construct proprietary stone profiles, architectural split-face reliefs, and signature chromatic blends. Bespoke master moulds can be prototyped, validated, and scaled to mass manufacturing within 14 calendar days.
Enterprise Buyer Priorities: Mitigating Supply Chain Risk
Commercial contractors, architectural specifiers, and high-volume stone distributors demand strict verification protocols before onboarding wholesale manufacturers.
Batch-to-Batch Color Reproducibility
For phased commercial developments spanning multiple years, chromatic stability across subsequent container shipments is non-negotiable. Advanced factories use digital spectrophotometers and mass-flow automated liquid pigment dispensing to guarantee delta-E values under 1.0 between production batches spaced quarters apart.
Export Packaging & Ocean Transit Integrity
Precast and artificial stone veneers suffer acute breakage if improperly packed. Enterprise buyers mandate heavy-duty fumigated pine crates reinforced with internal expanded polyethylene (EPE) corner protectors, vacuum-sealed barrier film, and cross-bracing capable of withstanding rough ocean transit and multi-tier warehouse stacking.
Guaranteed Production Lead Times
Supply chain bottlenecks halt job sites, triggering liquidated damages. Leading Chinese manufacturers mitigate this risk through substantial buffer stocks of dry ingredients, multi-lane casting tracks capable of producing 10,000 m² weekly, and flexible production scheduling to satisfy tight construction windows.
International Building Code Alignment & Localized Support
Ensure seamless installation sign-offs by deploying manufactured stone products verified against American, European, and Australasian civil engineering standards.
| Standard / Test Designation | Target Regulatory Region | Physical / Mechanical Attribute Tested | Factory Compliance Benchmark |
|---|---|---|---|
| ASTM C1670 / C1670M | North America (IBC / IRC) | Manufactured Stone Veneer Specification | Pass Density, absorption, compressive limit exceeded |
| ASTM E119 & UL 723 | North America | Fire Resistance & Surface Burning Characteristics | Class A Flame spread index: 0, Smoke development: 0 |
| EN 13501-1 | European Union (CE Marking) | Reaction to Fire Performance Classification | A1-s1, d0 Completely non-combustible material matrix |
| ASTM C482 | International Standard | Direct Flexural & Tensile Shear Bond Strength | > 0.35 MPa Excellent mortar adhesion to masonry backup |
| ASTM C67 (Modified) | Severe Climate Envelopes | Freeze-Thaw Resistance (50 Rapid Cycles) | < 1% Loss Zero disintegration, cracking, or surface scaling |
| ISO 9001 / ISO 14001 | Global Global Quality Standards | Environmental & Factory Quality Management | Certified Fully audited emissions, wastewater & QC tracing |
Engineered Architectural Application Typologies
From energy-efficient rainscreen retrofits to ultra-luxury residential hearths, artificial stacked stone provides versatile structural harmony across key sectors.
Commercial Building Facades & Rainscreens
Applied over cementitious backer board, metal studs, or cast concrete walls, lightweight artificial stacked stone ledger panels create striking visual weight without necessitating expensive footing enlargements or heavy masonry wall ties. Compatible with continuous exterior rigid insulation systems (EIFS/CI) to conform to ASHRAE 90.1 energy envelope parameters.
Multi-Family Residential & Master-Planned Communities
Developers of high-density subdivisions and mixed-use luxury apartment complexes utilize cultured stacked stone to establish warm regional vernaculars—ranging from California dry stack to European alpine rubble. Prefabricated panels accelerate trade installation speeds, reducing per-square-meter scaffolding duration by up to 40%.
Interior Architectural Features & High-Heat Fireplaces
Thanks to completely non-toxic, non-combustible mineral profiles, artificial ledger stone emits zero VOCs or toxic halogen gasses. It is specified universally for interior hotel reception accent walls, high-temperature gas or wood fireplace surrounds, residential basement wine cellars, and culinary feature pillars.
Industry Horizons: The Next Decade of Manufactured Veneer
Key evolutionary transformations shaping the artificial stone manufacturing domain through 2030 and beyond.
Low-Carbon Geopolymer Binders
In response to global Scope 1 & 2 industrial carbon reduction targets, next-generation formulations are supplanting traditional Portland cement with alkali-activated blast furnace slag and fly ash geopolymers, decreasing embodied manufacturing carbon by up to 45% without reducing yield hardness.
Ultra-Lightweight Polyurethane Composites
High-density structural PU and mineral-powder hybrid panels (weighing under 4.5 kg/m²) are carving out rapid market share in DIY consumer retail and modular pre-constructed container housing sectors where rapid mechanical screw installation replaces wet mortar techniques.
3D AI Scanning & Robotic Tooling
Photogrammetric LIDAR scanning of natural geological rock formations paired with 5-axis robotic mould milling allows factories to introduce hyper-realistic rustic stone series in record development cycles, capturing microscopic striations never before reproducible in precast media.
Nanotech Hydrophobic Self-Cleaning
Integration of nano-titania (TiO2) photocatalytic surface treatments into artificial stacked stone coatings enables solar-activated organic breakdown and superhydrophobic wash-off during natural rainfall, permanently resisting urban grime and atmospheric smog accumulation.
Frequently Asked Questions: Wholesale Procurement
Comprehensive answers compiled by our architectural engineering team regarding manufacturing, trade operations, and site performance.
What separates Tier-1 artificial stacked stone from cheap precast plaster?
How does artificial stone veneer compare to natural stone in total project costs?
What are typical Minimum Order Quantities (MOQs) and production lead times?
Can artificial stacked stone withstand extreme exterior freeze-thaw climates?
Which factory verification procedures are available for global importers?
What substrate preparation is required for exterior stone veneer installation?
Complementary Structural Granite, Slabs & Masonry Solutions
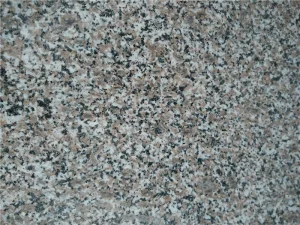
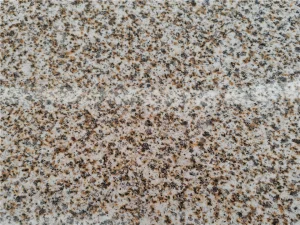
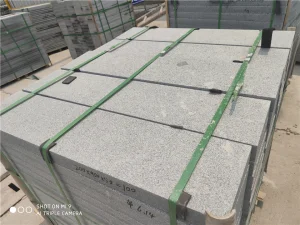
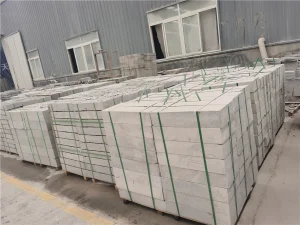
Direct from our Rizhao quarry processing facilities: select and combine manufactured veneer with heavy-traffic dimensional curbing, polished slabs, and paving stone modules.

Request Commercial Sample Boxes & Engineering Submittals
Partner directly with Rizhao Haichen Stone's engineering team for CAD takeoffs, ASTM test documentation, and customized factory-direct container quotes tailored to your structural project requirements.
