
Featured Artificial & Natural Stone Slab Portfolio (Part 1)
Direct factory catalog featuring engineered quartz, natural granite slabs, and structural facade tiles available for international bulk dispatch.
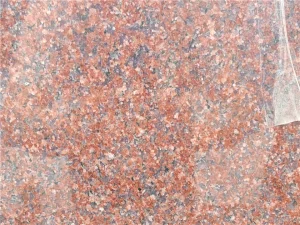
Wholesale G386 Shidiao Red Granite Tiles Manufacturers, Suppliers
View Specifications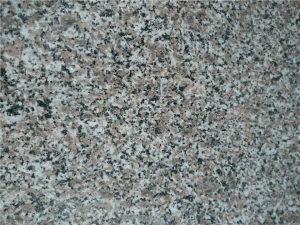
China G6361 Wulianhua Granite for Landscaping Manufacturer, Factories
View Specifications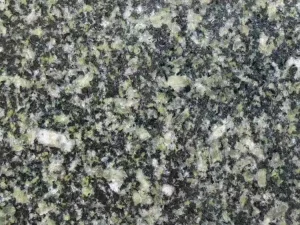
China G4101 Forest Green Granite Veneer Panels Supplier, Factories
View Specifications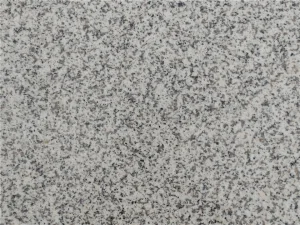
China G603 Sesame White Granite Suppliers, Factory
View Specifications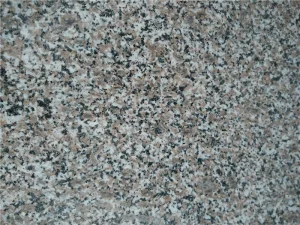
China Other Colours Granite – Custom Orders Manufacturers, Factories
View Specifications
Wholesale G654 Sesame Black Granite Polished Slabs Suppliers, Factories
View Specifications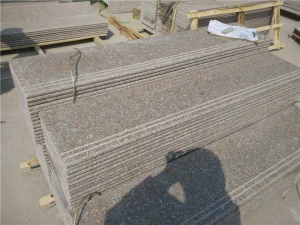
Wholesale G368 Wulian Red Granite Paving Stones Supplier, Suppliers
View Specifications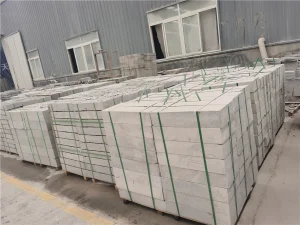
Wholesale Limestone Granite: Nature's Dual Gift Manufacturer, Factory
View Specifications1. Global Industrial Landscape & Macro Paradigm Shift in Artificial Stone Slabs
Analyzing market drivers, material evolution, and supply chain dynamics reshaping the B2B architectural surface sector.
Urbanization & Infrastructure
Rapid construction of commercial transit hubs, international airports, and modern medical centers demands ultra-durable flooring and wall cladding capable of handling high foot-traffic wear without mechanical degradation.
Natural Resource Conservation
Environmental regulations limiting open-pit natural quarrying have redirected major architectural procurement teams toward engineered stones that utilize up to 93% recycled mineral quartz, marble chips, and crushed feldspar.
Precision OEM Fabrication
Advanced 5-axis CNC machining, waterjet contouring, and automated edge-profiling require dimensionally uniform slabs free from natural fissures, internal micro-cracks, and structural color deviations.
2. Material Science & Production Methodology: Vibro-Compaction & Polymer Matrices
Deconstructing the internal chemistry, binder ratios, and high-vacuum compaction processes that define superior artificial slab performance.
Resin-Bonded Engineered Quartz (Bretonstone Process)
Comprising approximately 90% to 93% high-purity natural quartz aggregate (crystalline silica) combined with 7% to 10% unsaturated polyester resin, color pigments, and silane coupling agents. The mixture undergoes high-frequency vacuum vibro-compaction at pressures reaching 100 metric tons per square meter, followed by thermal curing in industrial kilns at 85°C–100°C.
- Flexural Strength: 40 – 55 MPa (ASTM C880)
- Porosity Level: Impermeable (< 0.03% water absorption)
- Chemical Resistance: Unaffected by household acids and alkaline cleansers
Inorganic Sintered Stone & Ultra-Compact Surfaces
Formulated strictly from 100% natural mineral bases including kaolin clay, feldspar, silica, and natural oxide pigments, synthesized without organic hydrocarbon resins. Sintered stone undergoes ultra-high pressing at 400 bar (40,000 kPa) and thermal sintering in roller kilns at temperatures exceeding 1,200°C (2,192°F).
- Thermal Resistance: Class A1 Non-Combustible (Direct flame resistance)
- UV Stability: 100% UV Weatherproof (Zero yellowing outdoors)
- Scratch Resistance: Mohs Scale 7–8 (Exceeds natural granite)
3. Technical Specification Matrix: Engineering Comparative Analysis
Rigorous ASTM and EN standard performance matrix comparing artificial stone slabs against conventional structural stones.
| Physical / Mechanical Property | Engineered Quartz Slabs | Sintered Artificial Stone | Engineered Marble Slabs | Natural Granite Slabs |
|---|---|---|---|---|
| Primary Composition | 93% Quartz Aggregate + Resin | 100% Natural Minerals (Sintered) | 90% Marble Dust + Resin/Cement | 100% Natural Igneous Rock |
| Density (ASTM C97) | 2.35 – 2.45 g/cm³ | 2.40 – 2.55 g/cm³ | 2.30 – 2.40 g/cm³ | 2.60 – 2.75 g/cm³ |
| Water Absorption (ASTM C97) | < 0.03% (Non-porous) | < 0.01% (Impermeable) | < 0.20% (Low) | 0.15% – 0.40% (Requires Sealing) |
| Flexural Strength (ASTM C880) | 45.0 – 58.0 MPa | 50.0 – 65.0 MPa | 18.0 – 25.0 MPa | 12.0 – 20.0 MPa |
| Mohs Hardness Rating | 6.5 – 7.0 | 7.0 – 8.0 | 3.0 – 4.0 | 6.0 – 6.5 |
| UV & Thermal Resistance | Indoor Only (< 150°C) | Full Outdoor (1200°C Resistant) | Indoor Only (< 100°C) | Full Outdoor Weathering |
| Dimensional Tolerance | ± 0.5 mm (Calibrated) | ± 0.3 mm (Precision CNC) | ± 0.5 mm | ± 1.5 mm – 2.0 mm |
4. Localized Application Scenarios & High-Performance Architectural Deployments
From healthcare cleanrooms to ventilated facade engineering—tailoring artificial stone slabs to severe structural environments.
Healthcare & Sterile Environments
In surgical operating theaters, pharmaceutical cleanrooms, and clinical laboratories, bacterial proliferation must be absolutely prevented. Engineered quartz and non-porous artificial slabs feature zero micro-capillaries, rendering them immune to blood, chemical reagent absorption, and microbial growth. Meets strict ISO 14644 cleanroom standards.
High-Traffic Commercial Flooring
International airport concourses, metro stations, and multi-story retail malls require floor coverings capable of enduring millions of high-heel and luggage wheel impacts per year. Jumbo artificial stone slabs (3200×1600mm) reduce grout joint frequency by 60%, minimizing maintenance costs while maximizing wear resistance.
Ventilated Rainscreen Facades
Extensively utilized in modern curtain-wall systems, 6mm and 12mm thin sintered artificial stone slabs provide exceptional flexural strength under severe wind-load conditions. Coupled with invisible undercut anchor mechanical fixing systems (Keil anchors), these slabs offer lightweight, fire-rated exterior envelope protection.
5. Global Regulatory Compliance, Low-Silica Standards & Quality Assurance
Navigating international health, safety, and environmental certifications for responsible wholesale procurement.
NSF 51 Food Contact Certification
Ensures artificial stone surfaces release zero volatile organic compounds, heavy metals, or toxic chemical residues when brought into direct contact with food preparation in commercial kitchens and restaurants.
GREENGUARD Gold Indoor Air Quality
Certifies extremely low total VOC emissions, making our artificial quartz and engineered slabs fully qualified for specification in educational buildings, hospitals, and LEED-certified green buildings.
CE Compliance (EN 15285 / EN 15388)
Mandatory European conformity documentation verifying compressive resistance, freeze-thaw durability, slip rating (PTV/R-ratings), and dimensional stability for public construction within the EU zone.
ISO 9001 & ISO 14001 Quality Management
Rigorous factory audits guaranteeing batch-to-batch color consistency, precise slab calibrating, zero internal voids, and environmentally sound wastewater recycling systems.
6. Industry 4.0 Technology Roadmap: AI-Driven Veining & Sustainable Bio-Resins
Exploring future technological breakthroughs shaping the artificial slab manufacturing ecosystem.
Full-Body 3D Digital Vein Injection
Traditional artificial stone often suffered from surface-only patterns. Next-gen production utilizes AI-guided multi-pass powder placement, extending natural marble veins fully through the 20mm and 30mm thickness of the slab, enabling authentic beveling and bullnose edges.
Plant-Based Bio-Resin Polymers
Replacing petroleum-based polyester resins with renewable plant-derived corn and soybean bio-resins reduces the carbon footprint per slab by up to 40%, enabling project developers to secure additional carbon credit points in environmental assessments.
Photocatalytic Self-Cleaning Surfaces
Integration of titanium dioxide (TiO₂) nano-particles into exterior artificial stone slabs creates photo-catalytic surfaces that decompose organic air pollutants under sunlight and wash clean naturally during rainfall events.
Featured Artificial & Natural Stone Slab Portfolio (Part 2)
Consolidated B2B supply of specialty stone varieties engineered for architectural facades, paving, and custom fabrication projects.
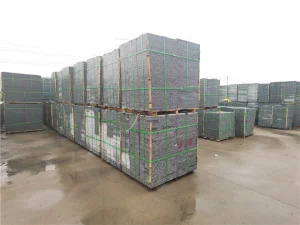
China G3702 Snowflake Blue Granite Manufacturers, Supplier
View Specifications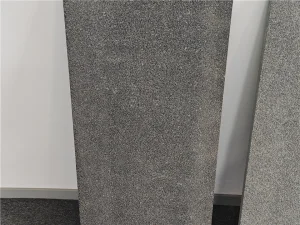
Wholesale G684 Fuding Black Granite Factories, Factory
View Specifications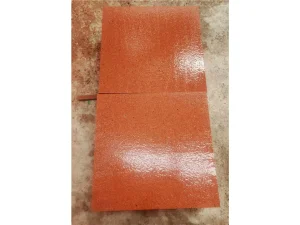
China Premium Chinese Red Granite Blocks Supplier, Suppliers
View Specifications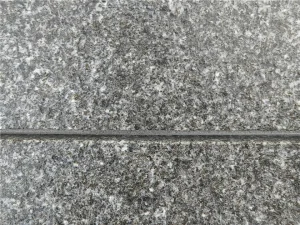
China G3701 Binzhou Blue Granite Suppliers, Factory
View Specifications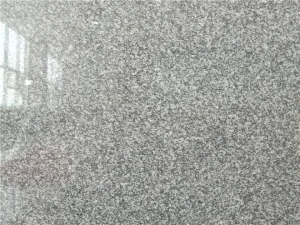
China G3743 Lu Grey Granite Building Stone Manufacturer, Factories
View Specifications
China A1684 Golden Hemp Granite Countertops Manufacturer, Factories
View Specifications
China G3401 Shanxi Black Granite Manufacturer, Factory
View Specifications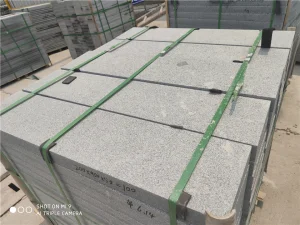
China G654 Sesame Grey Granite Flamed Finish Supplier, Factories
View Specifications7. B2B Global Supply Chain Architecture & Export Packaging Security
Ensuring pristine slab delivery across international sea routes via reinforced containerization and port-side logistics.
Heavy-Duty Heavy Steel A-Frames
Export slabs are strapped onto heavy-duty vertical steel or fumigated ISPM-15 wooden A-frames. Rubber padding strips separate each slab face to prevent scratching or polish dulling during wave-induced sea motion.
Port-Side Proximity (Rizhao / Qingdao)
Located within immediate proximity to Rizhao Port and Qingdao Port, our facility provides streamlined container stuffing, customs clearance, and reduced inland trucking freight fees for major shipping lines (Maersk, MSC, COSCO).
4-Stage Pre-Shipment Inspection
Every batch undergoes strict quality gates: 1) Ultrasonic flaw detection for internal voids; 2) Glossmeter evaluation across 9 points; 3) Thickness tolerance calibration; and 4) High-resolution photo/video signoff prior to container sealing.
8. B2B Technical Procurement FAQ: Answers for Specifiers & Importers
Expert technical clarity on slab dimensions, OEM fabrication, maintenance, and chemical durability.
