
Featured Natural Stone & Composite Formats
Quarry-direct slabs, precision composite elements, and custom architectural fabrications engineered for high-traffic commercial environments.

Architectural Whitepaper: The Evolution of Laminate Marble & Granite Table Manufacturing
In modern commercial architecture and contract furniture manufacturing, the structural paradigms governing stone dining tables, executive boardroom conference tops, and hospitality furniture have undergone a massive technological shift. Solid stone slabs, while traditionally valued for visual authenticity, present severe structural vulnerabilities: extreme deadweight load (often exceeding 65 kg/m² at 20mm thickness), susceptibility to flexural fracturing along natural vein fissures, and logistical cost bottlenecks.
What Defines Advanced Laminate Marble & Composite Tables?
A Laminate Marble Table represents a multi-layer material architecture combining ultra-thin real marble or high-pressure micro-calibrated stone veneers (3mm to 6mm) with engineered structural backings—such as structural aluminium honeycomb cores, high-density fiberboard (HDF), volcanic basalt substrates, or high-strength granite composite slabs. Manufactured under vacuum epoxy-resin bonding systems at pressures exceeding 150 N/cm², these composite structures deliver 300% higher flexural strength while reducing structural weight by up to 65% compared to legacy solid stone tops.
Technology Roadmap & Materials Science Outlook (2026–2032)
As global procurement mandates prioritize structural performance, carbon offset metrics, and mechanical reliability, our factory R&D division continuously advances stone laminating technologies.
Sub-surface Hydrophobic Nano-Ceramic Matrices
Traditional marble laminates suffer from micro-porous acid etching when exposed to acidic beverages or aggressive commercial cleaning agents. Next-generation production integrates vacuum-assisted organosilane nano-sealers that penetrate down to 2.5mm into the crystalline calcite grid, conferring zero-stain performance without altering natural tactile warmth.
Aluminium Honeycomb Substrate Fusion
Utilizing aerospace-grade 3003-H18 hexagonal aluminium cell cores sandwiched between dual fiberglass epoxy skins, laminate marble tops achieve ultra-lightweight performance (under 18 kg/m² for a 20mm total profile). This core eliminates dynamic deflection under high point-load stress in luxury restaurant and hotel banquet operations.
AI Vision-Guided Vein Matching & Profiling
Implementing multi-camera optical scanning arrays connected to 5-axis CNC diamond bridge saws allows automated grain continuity across multi-segment conference tables. Our factory algorithm predicts veining paths across stone blocks to yield bookmatched table sets with zero visual disruption.
China Factory 4.0: Supply Chain Resilience & Production Scale
Located in the heart of Shandong’s stone industrial cluster—Rizhao Haichen Stone Co., Ltd. integrates direct quarry extraction, block sawing, vacuum lamination technology, and immediate port access to deliver unmatched wholesale value.
Quarry-Direct Cost Advantage
By controlling direct raw material reserves including G602, G603, G654 Sesame Black, and Shandong White Marble/Granite, we eliminate middle-man margins. Raw stone blocks are processed on-site, cutting raw material transport costs by up to 25%.
Dual-Port Logistics Synergy
Our processing plant sits in close proximity to Rizhao Port and Qingdao International Deep-Water Port. This port-factory consolidation infrastructure shortens container staging times and enables direct FOB/CIF container shipping to Europe, North America, and the Middle East.
Scalable Automated Capacity
With multi-blade gang saws, automated slab calibrators, resin vacuum curing chambers, and waterjet edge fabricators, our facility achieves a monthly output exceeding 45,000 m² of composite stone panels and custom table components.
Commercial Segment Engineering Applications
Different commercial spaces demand specific technical specifications. Below is how our custom laminate marble and composite tables cater to global enterprise sectors:
Luxury Hospitality & Restaurants
High-turnover dining facilities require scratch-resistant, stain-impermeable surfaces capable of enduring thousands of hot dish contacts and cleaning cycles daily. Our ultra-thin marble fused to high-density composite backing provides luxury aesthetics without the cracking risks of traditional unreinforced marble tops.
Corporate Boardrooms & Executive Suites
Large-format executive conference tables spanning up to 4.5 meters in length are impossible to move or maintain in solid stone due to floor-loading limits. Lightweight marble laminates combined with honeycomb backings allow modular assembly, concealed wire raceways, and easy elevator transport.
Maritime & Luxury Cruise Interior Fit-Outs
Naval architecture strictly enforces bulk weight limits to maintain vessel stability and fuel efficiency. Our ultralight laminate stone tables comply with stringent marine weight-per-square-meter allowances while meeting IMO fire-retardant epoxy composite benchmarks.
Material Performance Matrix: Solid Stone vs. Composite Laminate Tables
Empirical physical properties based on standardized ASTM C615, ASTM C97, and EN 14617 testing criteria:
| Performance Metric | Solid Natural Marble (20mm) | Laminate Marble + Honeycomb (20mm) | Granite Base Composite Table (20mm) | Quartz Engineered Stone (20mm) |
|---|---|---|---|---|
| Average Surface Mass | 52 - 58 kg/m² | 16 - 20 kg/m² (-65%) | 48 - 54 kg/m² | 46 - 50 kg/m² |
| Flexural Strength (ASTM C880) | 8.5 - 12.0 MPa | 32.0 - 45.0 MPa (+300%) | 22.0 - 30.0 MPa | 16.0 - 24.0 MPa |
| Impact Resistance (Drop Test) | Low (Brittle fracture) | High (Absorbed by core) | High (Dense crystalline matrix) | Medium-High |
| Thermal Shock Tolerance | Medium (Risk of vein cracking) | High (Stabilized skin) | Very High (>250°C) | Low-Medium (Resin yellowing) |
| Stain Absorption Rate | 0.15% - 0.45% (High) | < 0.05% (Nano-sealed) | < 0.10% (Low) | < 0.03% |
| Logistics & Shipping Efficiency | High Freight Cost / High Breakage | Max Container Yield / Low Risk | Standard Freight Weight | Standard Freight Weight |
Global Enterprise Compliance & Localized Technical Support
Navigating international trade laws, structural codes, and green building environmental accreditations requires a fully verified manufacturing partner.
International Quality & Safety Compliance
All factory production runs are governed under strict ISO 9001:2015 Quality Management Systems and ISO 14001 Environmental Standards. Our products comply with European CE marking for structural cladding and stone countertops, NSF/ANSI Standard 51 for direct food contact safety, and US ASTM physical safety requirements.
LEED v4 & ESG Green Building Contribution
Laminate marble tables significantly lower raw quarry consumption by maximizing single-block yields up to 400% compared to thick slab cutting. Combined with zero-VOC epoxy adhesives and 100% recyclable aluminum or natural stone cores, our solutions contribute toward LEED v4 Low-Emitting Materials points.
Localized OEM/ODM & Project Support
We offer custom engineering support for commercial furniture brand owners, hotel procurement groups, and general contractors. Services include 3D CAD shop drawing validation, custom aluminum rim framing, dry-lay visual inspection photos/videos, and fumigated, heavy-duty sea crate packing.
6-Step Factory Production & Verification Protocol
Every batch of wholesale laminate marble and granite table components follows an audited, repeatable engineering lifecycle:
Quarry Block Selection
Raw stone blocks are visually inspected for structural integrity, minimal micro-cracking, and consistent color tone matching matching client-approved control samples.
Ultra-Thin Micro-Sawing
Precision diamond wire gang saws cut natural marble blocks into 4mm - 6mm thin veneer layers, followed by continuous thickness calibration scans.
Vacuum Resin Lamination
Veneers are fused to structural substrates (aluminum honeycomb, HDF, or granite slabs) using high-grade structural epoxy under heat-assisted vacuum curing presses.
CNC Edge Profiling
Automated 5-axis CNC router hubs carve bullnose, bevel, chamfer, or reverse-bevel table edge details directly to CAD project tolerances (±0.5mm).
Surface Sealing & Dry-Lay
Applying liquid-repellent nano sealers followed by a full dry-lay floor assembly to inspect pattern transitions across multi-piece contract table orders.
Export Container Packaging
Tops are foam-jacketed, edge-protected, and packed into ISPM-15 fumigated solid wood crates with internal shock-absorbing braces for safe maritime export.
Complementary Architectural & Table Material Options
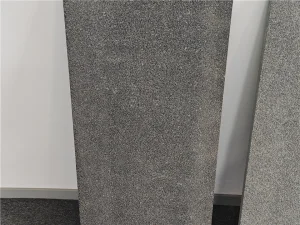
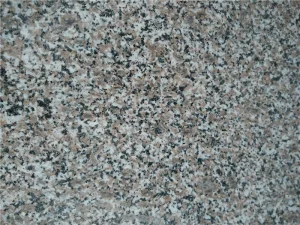
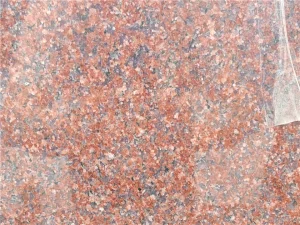
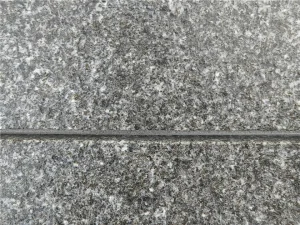
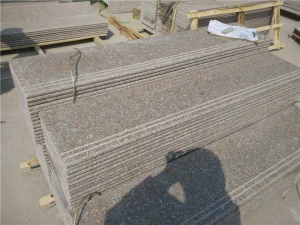
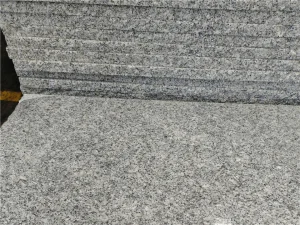
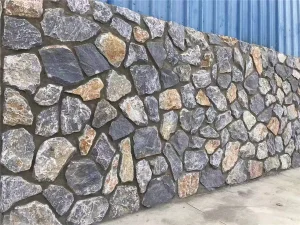
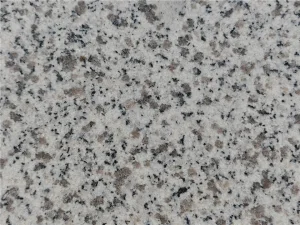
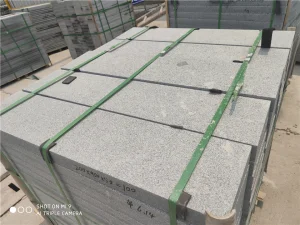
Select from our premium granite, dark marble, and specialty cut-to-size stones for custom contract table bases and top fabrications.
Wholesale Laminate Marble Table Manufacturers & Sourcing FAQ
Answers to critical technical, manufacturing, shipping, and quality assurance questions asked by international furniture importers, contract procurement teams, and commercial interior architects.
Request Engineering Specifications & Direct Factory Quotation
Partner with Rizhao Haichen Stone Co., Ltd. for your upcoming commercial table manufacturing, contract furniture program, or architectural project. Our trade and engineering team responds within 12 business hours.
