
High-Performance Architectural Stone Collections
Explore precision-calibrated cladding units, natural granite textures, and engineered stone veneer panels tailored for international distribution and contract delivery.
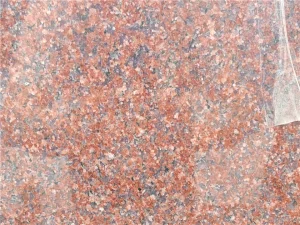
Wholesale G386 Shidiao Red Granite Tiles Manufacturers, Suppliers
View Specifications
Wholesale Limestone Granite: Nature's Dual Gift Manufacturer, Factory
View Specifications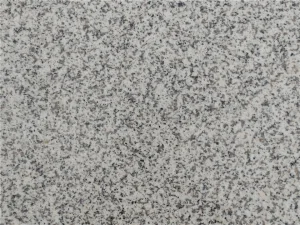
China G603 Sesame White Granite Suppliers, Factory
View Specifications
China A1684 Golden Hemp Granite Countertops Manufacturer, Factories
View Specifications
China G3401 Shanxi Black Granite Manufacturer, Factory
View Specifications
China G3701 Binzhou Blue Granite Suppliers, Factory
View Specifications
China Other Colours Granite – Custom Orders Manufacturers, Factories
View Specifications
China G654 Sesame Grey Granite Flamed Finish Supplier, Factories
View SpecificationsEngineering Paradigm of Modern Man-Made Stacked Stone
Decoupling dead-load constraints while maintaining authentic organic masonry aesthetics through advanced composite chemistry and polymer-modified casting matrices.
Lightweight Structural Load
Traditional quarry-cut stone imposes substantial dead loads ranging between 65 to 110 kg/m², necessitating fortified foundations, continuous structural ledges, and deep seismic ties. Modern engineered man-made stacked stone operates between 28 to 44 kg/m²—eliminating foundation footing requirements under IBC and IRC standard building codes.
- Eliminates secondary civil retrofits
- Reduces framing deflection tolerances
- Installs over wood-frame, cold-rolled steel, and ICF
Continuous Thermal Efficiency
Engineered stacked stone panels act as continuous composite thermal barriers. Formulated with lightweight aggregates such as expanded volcanic shale, perlite, and Portland hydraulic cement mixes, our ledger veneer yields an intrinsic R-value exceeding natural granite or basalt by up to 280%, decreasing envelope thermal bridging.
- Compatible with exterior EPS/XPS continuous insulation
- Eliminates condensation risk behind the wall plane
- Facilitates LEED v4 Energy & Atmosphere certification
Precision Z-Panel Interlock
Hand-dressing fieldstone incurs immense labor variability and elevated site installation costs. Haichen engineered veneer incorporates computerized Z-shaped interlocking module geometry with self-aligning horizontal stepped joints that obscure seam transitions while preventing water capillary intrusion into the substrate cavity.
- Modular 150×600 mm & 200×600 mm form-factors
- Dry-stack tight joints or grouted joints
- Zero-debris, high-speed on-site adhesive application
Localization Support, Quality Assurances & Global Compliance
Ensuring frictionless project approvals across North American, European, Middle Eastern, and Oceanic building jurisdictions through rigorous multi-standard laboratory qualification.
ASTM C1670 & ICC-ES AC51
Adhering explicitly to ASTM C1670 (Standard Specification for Adhered Manufactured Stone Masonry Veneer Units) and ICC-ES Acceptance Criteria AC51. Samples undergo regular third-party batch analysis verifying shear bond adhesive strength exceeding 0.35 MPa, ensuring fail-safe monolithic adhesion to polymer-modified Portland mortar bases.
- Tensile Bond Strength: ≥ 50 psi (ASTM C482)
- Water Absorption Threshold: ≤ 13% saturation
- Compressive Strength: ≥ 15 MPa (ASTM C192 / C39)
EN 15285 & CE Marking
For European Union and EEA markets, Haichen products conform fully to harmonized standards EN 771-5 (Manufactured Stone Masonry Units) and EN 15285. Full technical files, Declarations of Performance (DoP), and REACH chemical compliance certifications guarantee freedom from hazardous plasticizers, volatile emissions, and restricted heavy metal pigments.
- Reaction to Fire: Non-combustible Euroclass A1fl
- Thermal Shock Resistance: 50 cycles sans delamination
- Full traceability via QR-coded master carton lots
ASTM C67 Freeze-Thaw Integrity
Cold-climate resilience demands extreme freeze-thaw endurance. Subjected to 50 rapid freeze-thaw cycles under ASTM C67 and EN 1338 protocols, our engineered stacked stone matrix displays zero surface spalling, micro-fracturing, or mass degradation. The internal moisture network is chemically moderated by silane hydrophobic integrators.
- Weight Loss: < 0.5% after 50 intense freeze cycles
- Zero structural cleavage along decorative relief seams
- Optimized for Canadian, Nordic & Alpine conditions
| Test Parameter | Standard Reference | Standard Industry Requirement | Haichen Engineered Performance | Compliance Status |
|---|---|---|---|---|
| Compressive Strength | ASTM C192 / C39 | ≥ 12.4 MPa (1,800 psi) | ≥ 18.6 MPa (2,700 psi) | ✓ Compliant |
| Shear Bond Adhesion | ASTM C482 | ≥ 0.34 MPa (50 psi) | 0.58 MPa (84 psi) | ✓ Exceeds Code |
| Freeze-Thaw Resistance | ASTM C67 / EN 12371 | ≤ 1.0% mass loss / 50 cycles | 0.22% mass loss / No Cracks | ✓ High Latitude |
| Surface Burning Characteristics | ASTM E84 (UL 723) | Flame Spread ≤ 25, Smoke ≤ 450 | Flame Spread: 0, Smoke: 0 | ✓ Class A Fireproof |
| Density (Oven Dry) | ASTM C140 | ≤ 2,400 kg/m³ | 1,450 – 1,720 kg/m³ | ✓ Lightweight Spec |
China Factory Direct Supply Chain & Industrial Scale
Harnessing automated batching, precision silicone vacuum molding, and direct port connectivity to deliver uncompromised volume predictability and cost optimization.
Automated Micro-Dosing Casting
Our intelligent workshop utilizes computerized pneumatic batching to dispense aggregates, white Portland cement 52.5R, Bayer iron oxide pigments, and polymer admixtures with ±0.1% accuracy. Eliminating human batching errors guarantees exact tonal consistency across phased container orders spanning several calendar quarters.
- High-output continuous vibrating conveyor system
- Closed-loop computerized color slurry dispensing
- Daily production capacity: 3,500+ m² finished veneer
Silicone Vacuum Tooling
Surface authenticity originates from genuine natural master stones selected from our quarry blocks in Shandong. Master molds are reproduced using high-tear platinum vulcanized liquid silicone under vacuum de-aeration, capturing microscopic fissures, chiseled striations, and split-face geological grains that resist repetitive pattern detection.
- Over 300 unique master panel molds per series
- Subtle undercut depth reaching up to 45 mm
- Eliminates visual repeats across large-scale facades
Dual-Port Coastal Logistics
Situated in the Rizhao Stone Industrial Cluster, our manufacturing headquarters is located within minutes of Rizhao Port and under 120 km from Qingdao Port. This geographic consolidation enables dockside container drayage, bonded warehousing access, and zero transshipment handling, dramatically mitigating intermodal transit damages.
- FOB / CIF / DDP ocean freight routing
- Direct rail connections to Central Asian Silk Road
- Factory-managed phytosanitary wooden crating
Meeting Tier-1 Contractor, Architect & Distributor Demands
From private labeling and custom color-matching to site-ready pallet packaging, we engineer comprehensive sourcing ecosystems for commercial developers and bulk distributors.
OEM / ODM Private Labeling
We serve international distributors, tile wholesalers, and retail chains with complete OEM white-label packaging. High-tensile cardboard master boxes can be fully customized with private branding, EAN-13/UPC barcodes, QR installation instructions, and multilingual hazard data tailored to your target geographic market.
- Custom shrink-wrapping and moisture barriers
- Retail-ready drop-ship displays and merchandisers
- Comprehensive corner accessory box consolidation
Corner Units & Architectural Trims
Seamless execution requires precision monolithic accessories. We supply matching 90-degree interlocking corners, window keystones, sills, electrical utility outlet boxes, and pier caps fabricated using identical stone matrices to eliminate color differentials and messy 45-degree site miter joints.
- L-shaped corner panels for rapid structural wrapping
- Water-shedding sloped wainscot sills
- Precision matching mantels & hearth stones
LEED v4 & ESG Procurement
Engineered stone satisfies stringent corporate sustainability thresholds. By incorporating up to 35% post-industrial recycled granite aggregates, slag, and zero-VOC mineral pigments, project specifiers secure vital points under LEED v4 Materials and Resources (MR) credits and BREEAM environmental ratings.
- Recycled content verification documentation
- Zero volatile organic compound (VOC) off-gassing
- Non-toxic mineral composition (silica-safe handling)
Technological Evolutions in the Man-Made Stacked Stone Sector
Emerging chemical formulations, dry-hung mechanical installation channels, and biophilic architectural trends reshaping the masonry horizon.
Polyurethane Ultra-Light Panels
Next-generation lightweight engineered stone utilizes closed-cell high-density polyurethane (PU) formulations with inorganic mineral protective coatings. Achieving an ultra-light mass under 4.5 kg/m², these panels screw directly onto plywood sheathing or metal furring channels without mortar, ideal for high-rise retrofits.
- Weather-independent sub-zero installation
- R-value rating up to R-4.5 per inch thickness
- Significant reduction in transoceanic freight cost
Dry-Hung Ventilated Façades
Modern commercial specifications increasingly demand rainscreen engineering. Haichen has introduced engineered stone panels with embedded stainless steel clip slots, enabling mechanical anchoring onto aluminum sub-framing. This architectural method creates continuous air cavities that evaporate moisture and mitigate solar heat gain.
- Seismic safety compliant under ASCE 7-16
- No wet trades or temperature curing restrictions
- Permits modular panel replacement for building maintenance
Biophilic & Modernist Colorways
Architectural preferences have shifted decisively toward deep monochromatic palettes and refined textures. Haichen R&D specializes in crisp arctic whites, slate charcoals, and iron-sand oxidized patinas that merge raw organic masonry geometry with minimalist Scandinavian and modern industrial elevations.
- Linear dry-stack profiles with sharp chiseled relief
- Zero UV-fading via inorganic ceramic-fired pigments
- Custom architectural color development within 7 days
Versatile Installation Typologies in Modern Construction
Engineered stacked stone panels bridge the boundary between heavy structural civil facades and refined interior accent wall statements.
Exterior Façades & Wainscoting
Designed for exterior residential and commercial building envelopes. Integrates seamlessly with drainage planes, cement backer boards, and masonry substrates to elevate perimeter curb appeal while withstanding wind-driven rain, UV exposure, and thermal shock.
Fireplace Surrounds & Hearths
With an ASTM E84 Class A non-combustible certification, our cast stone panels withstand elevated temperatures without emitting smoke, toxic odors, or suffering structural matrix deterioration around zero-clearance gas or wood fireplaces.
Hospitality & Interior Accents
Interior feature walls in hotel lobbies, corporate headquarters, and high-end restaurants benefit from the acoustic sound-scattering facets of stacked stone. The lightweight profile allows direct mounting over reinforced drywall.
Retaining Walls & Landscape Piers
Enhancing concrete block landscape walls, outdoor barbecue kitchens, and entry monuments. Chemical weatherization barriers prevent efflorescence bloom when subjected to constant outdoor soil moisture and irrigation overspray.
Frequently Asked Questions for Project Engineers & Buyers
Comprehensive answers regarding chemistry, certifications, structural installation, container logistics, and factory capabilities.
What is the exact material formulation of Haichen man-made stacked stone?
How does man-made stacked stone perform under severe freeze-thaw cycles?
Does man-made stone veneer require structural foundation wall ties or ledges?
Will color pigments fade, leach, or degrade when exposed to prolonged sunlight?
What is the minimum order quantity (MOQ) and production turnaround for full containers?
How is cargo breakage controlled during transpacific and deep-sea maritime transit?
Can Haichen replicate custom architect samples or competitor color lines?
Premium Natural & Fabricated Cladding Stone Units
Complete project packages: coordinate engineered stacked veneers with natural granite accents, dimensional building masonry, and quarry-direct architectural elements.
Wholesale G3760 Shandong White Marble Granite Manufacturers, Suppliers
View Specifications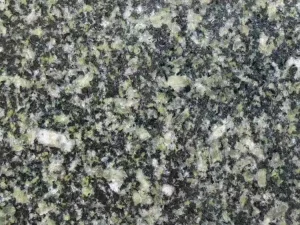
China G4101 Forest Green Granite Veneer Panels Supplier, Factories
View Specifications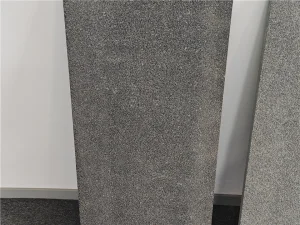
Wholesale G684 Fuding Black Granite Factories, Factory
View Specifications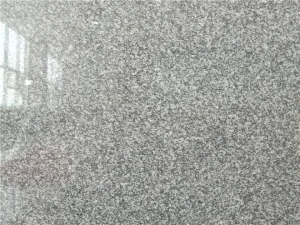
China G3743 Lu Grey Granite Building Stone Manufacturer, Factories
View Specifications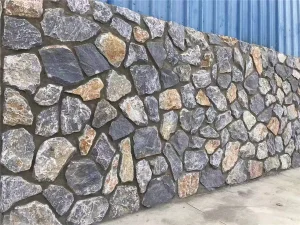
Wholesale Chinese Culture Granite: Stone Chronicles a Millennium, Artistry Inherits the Orient Manufacturer, Suppliers
View Specifications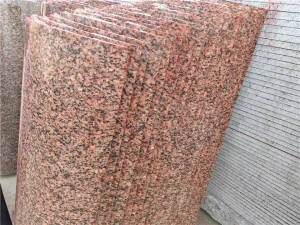
Wholesale G352 General Red Granite Cladding Panels Manufacturers, Factories
View Specifications
China G3702 Snowflake Blue Granite Manufacturers, Supplier
View Specifications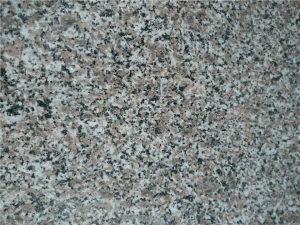
China G6361 Wulianhua Granite for Landscaping Manufacturer, Factories
View SpecificationsQuality Control Protocols: Six-Stage Plant Inspection
From micro-aggregate sizing to final pallet moisture checks, every panel batch is monitored via automated sensory arrays and QA laboratory verification.
1. Spectrophotometric Color Matching
Every pigment lot is cross-calibrated against master delta values under standardized D65 daylight lamps. Color variation is restricted within ΔE ≤ 0.7 to avoid noticeable visual shifts between separate manufacturing shifts.
2. Laser Dimensional Calibration
Automated optical scanning systems measure the height, width, and interlocking edge perpendicularity of every demolded panel. Dimensional deviation is constrained within ±1.0 mm, guaranteeing seamless site butt joints without field cutting.
3. Hydrostatic & Bond Shear Auditing
Randomly selected batch specimens undergo rigorous destructive testing for internal voids, flexural elasticity, and mortar bond pull-off shear. Any panel showing internal micro-porosity pockets above 2.5% is rejected.
