
Featured Architectural Stone Solutions (Part I)
Precision-machined natural granite slabs, tiles, and stacked ledge veneer components sourced directly from our Shandong production facilities.
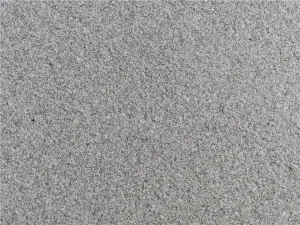
China G614 Sesame Grey Granite Slabs & Tiles
View Product Specs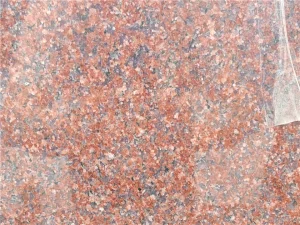
Wholesale G386 Shidiao Red Granite Tiles
View Product Specs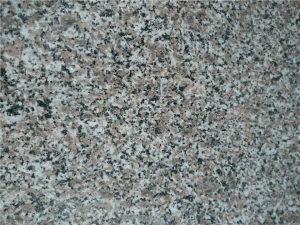
China G6361 Wulianhua Granite for Landscaping
View Product Specs
China A1684 Golden Hemp Granite Countertops
View Product Specs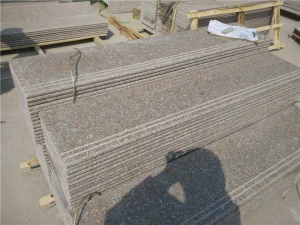
Wholesale G368 Wulian Red Granite Paving Stones
View Product Specs
China G3701 Binzhou Blue Granite Facade Slabs
View Product Specs
China G3702 Snowflake Blue Architectural Stone
View Product Specs
Wholesale G684 Fuding Black Granite Blocks
View Product SpecsGlobal Commercial & Industrial Landscape of Stacked Rock Fireplaces
The international demand for manufactured natural stone cladding and stacked rock fireplace surrounds has experienced a structural shift. Driven by architectural preferences for biophilic interior design, rustic modernism, and zero-clearance outdoor heating elements, high-volume real estate developers and commercial stone distributors are increasingly sourcing pre-panelized natural stone systems directly from primary processing hubs.
The global natural stone veneer and fireplace surround market is projected to expand at a CAGR of 6.4% through 2030. Commercial multi-family developments, luxury hospitality resorts, and high-end suburban residential projects account for over 68% of volume shipments from OEM factories.
Traditional mason-installed unit-by-unit stone construction has largely yielded to standardized interlocking Z-shaped and S-shaped stacked rock panels. Pre-assembled panels reduce field installation labor overhead by up to 70% while eliminating dimensional drift across expansive multi-story hearths.
Leading manufacturing factories are adopting closed-loop water recycling systems and zero-VOC mineral adhesives. Modern stacked rock fireplace products comply fully with USGBC LEED v4.1 indoor air quality thresholds and global thermal performance standards.
For commercial importers and distributor purchasing directors, securing direct relationships with quarry-integrated factories like Rizhao Haichen Stone Co., Ltd. eliminates middleman price distortion, guarantees color tone consistency across multi-container production runs, and provides structural warranty backed by lab-certified compressive strength data.
Technical Fabrication Roadmap & Automated Manufacturing
Producing high-grade stacked rock fireplace veneer panels at industrial scale requires a fusion of raw quarry management and state-of-the-art CNC stone-cutting technology. Our Shandong manufacturing facility utilizes automated diamond multi-wire saws, hydraulic split-face machines, and thermal shock curing lines to engineer veneer panels that meet exact architectural specifications.
Raw granite, quartzite, and slate blocks are split into consistent substrate slabs using computerized gang saws. Automated calibrating rollers maintain slab thickness tolerances within ±0.5 mm, preventing step-offs when panels are dry-fitted during high-density installation.
Hydraulic splitters exert targeted pressure along natural geological cleavages, generating authentic tactile split-face textures. Individual stone strips are cut into calibrated depths ranging from 15 mm to 35 mm to create dimensional relief across the fireplace face.
Stone strips are arranged into 600×150 mm or 600×200 mm Z-panel templates. Depending on specification, strips are joined using industrial structural polyurethane epoxy, fiberglass mesh, or cementitious backing reinforced with stainless steel clips for elevated thermal environments.
Finished panels pass through automated thermal cycling chambers simulating extreme fireplace temperature shifts (up to 300°C / 572°F continuous exposure). Every batch undergoes laser dimensional verification and color-matching dry-lay assembly prior to export packing.
System Comparative Analysis: Stacked Rock Materials
| Material System Type | Primary Composition | Fire Resistance Rating | Thermal Mass Retention | Lifespan Expectancy | Maintenance Profile |
|---|---|---|---|---|---|
| Natural Granite / Quartzite Stacked Panel | 100% Crystalline Natural Stone | Class A1 Non-Combustible (>1000°C) | Superior (High Thermal Mass) | 100+ Years | Minimal (Penetrating Sealer optional) |
| Pre-Cast Concrete Simulated Stone | Portland Cement, Aggregates, Pigments | Class A1 Non-Combustible | Moderate | 20–30 Years (Fading risk) | Periodic Resealing & Recoloring |
| Polyurethane Synthetic Faux Rock | High-Density Polyurethane Foam | Class B / C (Combustible above 80°C) | Negligible (Insulator) | 10–15 Years (Indoor only) | Vulnerable to Heat Deformity |
| Direct-Cut Thin Stone Ledger Strips | Solid Natural Slate / Marble | Class A1 Non-Combustible | High | 75+ Years | Low Maintenance |
Macro Industry Solutions & Localized Application Scenarios
Fireplace architecture varies significantly across global climate zones, regional building codes, and aesthetic trends. As an enterprise manufacturer, Haichen Stone provides customized macro solutions adapted to regional installation parameters.
In the United States and Canada, linear wide-format gas fireplaces and high-BTU wood-burning stoves demand cladding materials that exhibit absolute zero flame spread (ASTM E84 Class A). Our G614 Sesame Grey and G684 Fuding Black stacked rock panels are engineered with recessed mechanical anchor slots, allowing rapid tie-in to heavy-duty steel framing without structural deflection.
- Compliant with IRC (International Residential Code) clearance-to-combustible rules.
- Resistant to severe freeze-thaw cycles in alpine regions (Rocky Mountains / Midwest).
European urban developments favor high thermal efficiency bioethanol units and compact pellet stoves. Substrate weight is a critical engineering bottleneck in historical building retrofits. We produce lightweight 15-20 mm calibrated G602 & G603 Sesame White ledger panels that reduce dead weight load on floors while preserving real natural stone texture.
- Full CE marking compliance under EN 1469 & EN 12057 standards.
- Zero chemical outgassing when exposed to radiant heating elements.
Luxury hospitality resorts in Dubai, Riyadh, and Doha require outdoor open-air fire pits and feature walls that endure aggressive thermal expansion contrast between intense daytime sun and nighttime fire heating. Our dense igneous granites (such as G3701 Binzhou Blue and G386 Shidiao Red) resist thermal cracking and salt-air corrosion in coastal installations.
- Tested against extreme UV degradation and thermal shock up to 80°C delta T.
- Non-porous crystalline structure prevents sand dust impregnation.
Commercial developments across Tokyo, Singapore, and Sydney utilize stacked stone fireplaces as architectural central anchors in grand hotel lobbies and penthouse suites. Our factory supplies custom pre-corner pieces ("L-shaped corner panels") that eliminate exposed joint seams, producing a seamless, solid-masonry appearance on 90-degree outer return walls.
- Includes pre-matched 90° interlocking corner elements for clean edge detailing.
- Flexible batch sizing tailored to mixed-use high-rise logistics schedules.
Technical Specifications & Standard Performance Data
All stacked rock products manufactured by Rizhao Haichen Stone Co., Ltd. undergo standardized physical laboratory testing in accordance with ASTM C615 / C97 / C170 and European Norm EN 1341 certifications.
| Physical Property | Testing Standard | Granite Ledger Value | Slate Ledger Value | Quartzite Ledger Value |
|---|---|---|---|---|
| Bulk Density (kg/m³) | ASTM C97 / EN 1936 | 2,620 – 2,750 kg/m³ | 2,700 – 2,800 kg/m³ | 2,650 – 2,720 kg/m³ |
| Water Absorption (% by wt.) | ASTM C97 / EN 13755 | 0.15% – 0.32% | 0.20% – 0.45% | 0.10% – 0.25% |
| Compressive Strength (MPa) | ASTM C170 / EN 1926 | 140 – 210 MPa | 120 – 180 MPa | 160 – 230 MPa |
| Flexural Strength (MPa) | ASTM C880 / EN 12372 | 14.5 – 22.0 MPa | 16.0 – 25.0 MPa | 18.0 – 28.0 MPa |
| Freeze-Thaw Resistance | EN 12371 (100 Cycles) | No Loss of Integrity | No Loss of Integrity | No Loss of Integrity |
| Fire Safety Reaction | EN 13501-1 / ASTM E84 | Class A1 / Flame Spread 0 | Class A1 / Flame Spread 0 | Class A1 / Flame Spread 0 |
| Standard Panel Dimensions | Factory QC Spec | 600×150×15-25 mm | 600×150×12-20 mm | 600×150×15-30 mm |
Enterprise Supply Chain Protocol & Quality Control Workflow
We manage every link of the supply chain—from initial quarry seam selection to container loading at nearby Rizhao and Qingdao sea ports. Our rigid 6-stage Quality Management System guarantees that international shipments arrive undamaged, dimensionally consistent, and ready for immediate jobsite installation.
Blocks are evaluated directly at our Shandong quarry faces for structural density, consistent color graining, and absence of micro-fractures prior to transport to our sawmills.
Multi-blade diamond saws trim split stone into exact height bands (e.g., 20mm, 30mm, 50mm height variations) to ensure balanced visual layering on every assembled panel.
Technicians perform full batch dry-lays across 50 m² floor sections under calibrated daylight lamps to filter out severe tonal variances and verify inter-panel fitment.
Bond strength between stone backing substrate and individual strips is pull-tested to exceed 1.5 MPa, ensuring zero strip detachment during shipping transit or thermal expansion.
Panels are packed into corrugated inner boxes lined with high-density EPE foam, then loaded into export-grade, IPPC-certified fumigated hardwood crates with steel corner strapping.
Direct proximity to Rizhao Port and Qingdao Port allows fast container dispatch, real-time GPS tracking, and complete export customs clearing documentation for overseas clients.
Frequently Asked Questions (FAQ) for Enterprise Wholesale Buyers
Detailed answers regarding manufacturing capabilities, minimum order quantities (MOQ), custom OEM fabrication, thermal safety compliance, and global delivery terms.
What is the distinction between natural stacked rock veneer and manufactured concrete stone?
Natural stacked rock veneer panels are manufactured from 100% genuine quarried granite, slate, or quartzite. Unlike manufactured concrete stone (which uses painted cement cast in silicone molds), natural stone will never fade under heat exposure or intense sunlight, exhibits zero efflorescence, offers higher compressive strength, and possesses an authentic geological texture.
Are stacked rock fireplace panels suitable for high-heat wood-burning fireplaces?
Yes. All natural granite, slate, and quartzite stacked panels produced by Haichen Stone are rated Class A1 non-combustible. They tolerate continuous surface temperatures well over 500°C (932°F) without cracking or emitting smoke. For firebox interiors, firebricks must be used, but for outer surround fascia and chimney breast cladding, our stacked panels provide optimal structural performance.
What is your Minimum Order Quantity (MOQ) for custom architectural orders?
Our standard MOQ for wholesale distributor orders and commercial project packages is one 20-foot full container load (FCL), which yields approximately 400 to 650 square meters (4,300 to 7,000 sq.ft) of ledger panels depending on stone thickness. We also support mixed-color container loads allowing buyers to combine multiple granite and slate finishes.
How do you supply matching corner pieces for 90-degree fireplace returns?
We fabricate dedicated L-shaped corner panels ("Interlocking 2-piece Corner Sets" or "Pre-glued 90° Mitered Corners"). These pieces allow installers to wrap fireplace columns and chimney returns seamlessly, hiding end-grain seams and replicating the appearance of thick full-bed stone masonry.
What adhesive and installation substrate systems are recommended?
Stacked rock panels should be installed over cement backer board (such as Durock or HardieBacker), unpainted masonry, or scratch-coat wire lath using a modified polymer thin-set mortar (conforming to ANSI A118.4 or EN 12004 C2TE standards). For installations exceeding 3 meters in height, mechanical anchoring clips embedded into the stone backing are recommended.
Can Haichen Stone execute custom OEM sizes and private label packaging?
Yes. We regularly manufacture custom OEM ledger dimensions (such as 150×600mm, 200×600mm, or 180×350mm) according to client blueprints. Furthermore, we provide full private label packaging—printing distributor logos, barcoding, and localized installation manuals directly on cardboard carton boxes.
What are the sea freight lead times and Incoterms offered?
Standard manufacturing lead time for 1–3 FCL containers is 15 to 25 days from deposit confirmation. Shipping from Rizhao Port or Qingdao Port to North American west coast ports takes approximately 14–18 days; European main ports 28–35 days; Middle East ports 18–22 days. We routinely execute orders under FOB, CFR, CIF, and DDP Incoterms.
Featured Architectural Stone Solutions (Part II)
Explore our broader catalog of natural granite, sesame white pavers, black obsidian blocks, and oriental cultural architectural stone components.
China G603 Sesame White Granite Slabs
View Product Specs
Wholesale G602 Sesame White Granite Tiles
View Product Specs
China G3401 Shanxi Black Granite Blocks
View Product Specs
Wholesale G654 Sesame Black Polished Slabs
View Product Specs
China Premium Chinese Red Granite Blocks
View Product Specs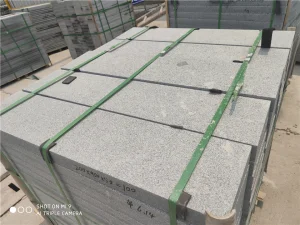
China G654 Sesame Grey Flamed Stone
View Product Specs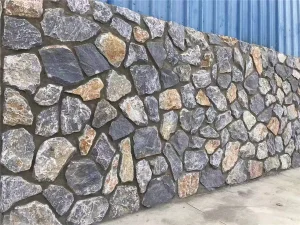
Wholesale Chinese Culture Granite Stone
View Product Specs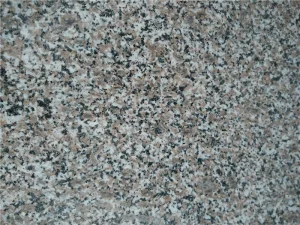
China Custom Color Granite Orders
View Product SpecsAccelerate Your B2B Natural Stone Procurement
Partner directly with Rizhao Haichen Stone Co., Ltd. for factory-direct pricing, certified material quality, and reliable global containerized shipping. Contact our international trade engineering desk to request physical sample boxes, CAD shop drawings, or factory audit schedules.
