
Quarry-Direct Natural Granite & Stone Catalog
Explore our primary export-grade dimensional stone selections engineered for high flexural performance and architectural elegance.
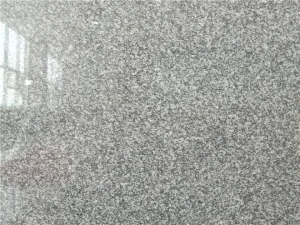

China Moonlight White Granite in Global Architecture
Analyzing the industrial evolution, petrographic superiority, and procurement strategy for Chinese white granite.
In contemporary architectural design and urban civil engineering, selecting appropriate cladding and paving materials requires balancing aesthetic luminosity, structural integrity, and long-term economic efficiency. China Moonlight White Granite—geologically categorized within the fine-to-medium grained quartz-feldspar plutonic formations of Shandong Province—has emerged as a foundational benchmark material in global construction. Often specified under codes such as G3760 or referenced alongside regional variants like Shandong Pearl White, this stone bridges the aesthetic warmth of classic Italian white marbles with the indestructible mechanical resilience inherent to high-grade crystalline granite.
The global natural stone market has undergone a significant structural shift. As sustainable building frameworks (such as LEED v4.1 and BREEAM) penalize high-embodied-carbon synthetic products like engineered quartz or resin-bound composites, natural dimension stone sourced directly from zero-waste automated quarries has regained dominant market share. China Moonlight White Granite manufacturers have led this industrial modernization, integrating digital block-scanning, diamond wire-saw extraction, and circular water-treatment infrastructure to deliver cut-to-size panels with millimetric dimensional accuracy.
Quarry Reserves & Integrity
Extracted from rich, consolidated batholiths in Shandong, ensuring massive block extraction capacity with consistent microcline color purity and minimum tonal variation across 100,000+ m² facade contracts.
Freeze-Thaw Weathering
Near-zero water absorption (<0.22%) prevents interstitial ice expansion, making Moonlight White Granite immune to spalling, micro-fracturing, and salt-crust efflorescence in harsh Northern European and North American climates.
High-Efficiency Fabrication
Utilizing multi-blade gang saws and 5-axis CNC routing systems, Chinese suppliers deliver high-precision cut-to-size cladding, radial kerbstones, and polished internal flooring with minimal lead times.
Petrographic Profile & Engineering Benchmarks
Rigorous physical test parameters validated under ASTM C615 and European Standard EN 1469 requirements.
Petrographically, China Moonlight White Granite is classified as a leucocratic granodiorite. The mineralogical matrix comprises predominantly Plagioclase Feldspar (48–52%), Quartz (30–35%), Microcline (10–14%), and trace amounts of Biotite and Muscovite (3–5%). The interlocking crystal lattice provides exceptional compressive strength, enabling thin-cut 20mm panels to perform reliably in back-ventilated dry-hung curtain wall assemblies under extreme wind-load forces.
| Physical / Mechanical Property | Test Standard | Industry Baseline | China Moonlight White Standard |
|---|---|---|---|
| Bulk Density (g/cm³) | ASTM C97 / EN 1936 | ≥ 2.56 g/cm³ | 2.65 - 2.68 g/cm³ |
| Water Absorption (%) | ASTM C97 / EN 13755 | ≤ 0.40 % | 0.18 - 0.22 % (Superior Hydrophobic) |
| Compressive Strength (Dry, MPa) | ASTM C170 / EN 1926 | ≥ 131 MPa | 168 - 182 MPa |
| Flexural Strength (Rupture, MPa) | ASTM C880 / EN 12372 | ≥ 8.6 MPa | 13.5 - 15.2 MPa |
| Abrasion Resistance (mm) | ASTM C241 / EN 14157 | ≤ 25 mm | 14.2 mm (High Foot-Traffic Grade) |
| Slip Resistance (Flamed Finish, SRV) | EN 14231 / BS 7976 | ≥ 36 Wet | 68 - 74 Wet (Maximum Safety) |
| Acid & Alkali Resistance | GB/T 17670 | Class B | Class A (Non-reactive to acid rain) |
Engineering Technical Note for Structural Specifiers
Due to its low coefficient of thermal expansion (approx. 6.5 x 10^-6 /°K), China Moonlight White Granite exhibits minimal expansion joints requirements in large-scale exterior plaza layouts. When designing curtain walls with undercut anchor brackets (such as Fischer or Keil systems), the high flexural strength (14+ MPa) allows reduction of panel thickness from 30mm down to 20mm without compromising structural safety margins under ASTM E330 wind loads.
Quarry-to-Site Manufacturing & Quality Assurance
How modern Chinese stone factories leverage Industry 4.0 automation to eliminate surface defects and shade discrepancies.
1. Spectrophotometric Color Matching
Natural stone inherently features slight microcline variations. Leading China Moonlight White Granite suppliers employ automated camera vision systems and digital spectrophotometers during slab calibration. Slabs are sorted into sub-shading batches (Delta E < 0.5) to guarantee continuous optical uniformity across adjacent facade panels on site.
2. Precision Surface Finish Technology
Depending on architectural intent, processing lines apply customized textures:
- High-Gloss Polished (90+ Gloss Units): Ideal for executive interior lobbies, feature walls, and vanity counters.
- Flamed & Waterjet Brushed: High-temperature thermal treatment followed by high-pressure waterjet cleaning creates a smooth, slip-resistant exterior surface.
- Bush-Hammered (Litchi Surface): Uniform mechanically pitted texture designed for municipal ramps and high-traction plazas.
3. Automated Dry-Lay & Pre-Assembly Audit
For complex architectural blueprints involving curved profiles or intricate stone carving, Chinese manufacturers conduct factory dry-lays. Panels are laid out across factory floors according to shop drawings, numbered, scanned via QR code, and video-inspected by the client's QA engineers prior to fumigated wooden crate packaging.
4. Port-Factory Logistics Integration
Situated within close proximity to major international shipping hubs like Qingdao Port and Rizhao Port, suppliers offer streamlined FOB, CIF, and DDP export logistics. Heavy-duty fumigated wooden crates lined with waterproof membrane film prevent ocean-transit moisture absorption and rust staining.
Sustainable Quarrying & Green Building Contribution
Quantifiable environmental metrics driving decarbonization across modern architectural material selection.
Architectural Applications & Material Comparison
Comparative evaluation of China Moonlight White Granite against alternative facade and flooring substrates.
Ventilated Rainscreen Facades
Specified extensively in high-rise corporate headquarters and civic museums. Mounted via aluminum dry-hanging sub-frames with stainless steel pin anchors, providing thermal insulation backings and severe weather envelope resistance.
Transit Hub Pedestrian Paving
Flamed and bush-hammered tiles (30mm, 50mm, or 80mm thickness) withstand high dynamic wheel loads from maintenance vehicles and heavy foot traffic in international airport concourses and metro terminals.
Interior Luxury Countertops & Flooring
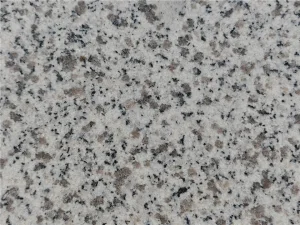
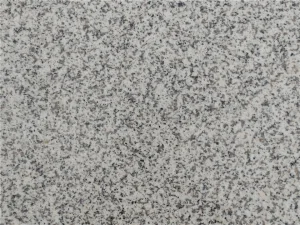
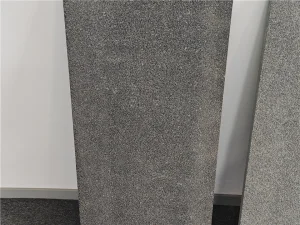
Polished slabs showcase a crisp white background peppered with soft grey quartz crystals, providing stain-resistant, scratch-proof kitchen worktops, vanity tops, and hotel lobby flooring.
Material Trade-off Matrix: Granite vs. Competitors
| Evaluation Parameter | China Moonlight White Granite | Natural White Marble (Carrara/Volakas) | Porcelain / Sintered Stone Slabs |
|---|---|---|---|
| Hardness (Mohs Scale) | 6.5 - 7.0 (Highly Scratch Resistant) | 3.0 - 4.0 (Prone to scratching) | 6.0 - 7.0 |
| Acid Stain Susceptibility | Immune to household acids/lemon/rain | High etching risk from mild acids | Immune |
| Impact Resistance (Joules) | High structural toughness | Medium / Brittle | Low edge impact resistance (Chipping) |
| Thermal Expansion / Thermal Shock | Stable under extreme climate swings | Susceptible to micro-cracking | Can crack under intense point heat |
| Project Lifecycle Cost (30 Yr) | Lowest (Zero maintenance required) | High (Frequent sealing/polishing) | Medium (Requires structural re-grouting) |
Technical Roadmap & Future Engineering Horizons
Innovations shaping lightweight stone composite systems and digital stone fabrication from 2025 to 2030.
Ultra-Thin Composite Panel Technology
To address the weight limitations of mega-tall building structures, Chinese research institutes and manufacturers are pioneering lightweight Granite-Aluminum Honeycomb Panels. By bonding a 5mm veneer of China Moonlight White Granite to a 15mm aircraft-grade aluminum honeycomb backing, panel weight is reduced by up to 65% (from 80 kg/m² down to ~22 kg/m²) while increasing impact strength by 300%.
This innovation enables rapid retrofitting of legacy commercial buildings without structural foundation reinforcement and significantly lowers ocean freight shipping costs per square meter.
5-Axis CNC Waterjet & Carving Automation
Advanced fabrication plants in Shandong are incorporating AI-driven 5-axis CNC routers and robotic carving arms. Complex architectural capitals, curved radius curbings, 3D textured feature walls, and intricate heritage monument restorations can now be machined directly from 3D CAD files with sub-millimeter tolerances.
This hybrid approach combines traditional oriental stone masonry art with modern digital precision, reducing custom production lead times from months to days.
International Certification & Logistics Protection
Ensuring zero-claim deliveries across European, North American, Middle Eastern, and Asia-Pacific markets.
CE Marking & EN Standards
Full compliance with European Union Construction Products Regulation (CPR). Certified test reports for EN 1469 (Slabs for cladding) and EN 1341 (Slabs for external paving) provided with every shipment.
ASTM C615 Testing Verification
Regular third-party laboratory audits (SGS / Intertek) confirming compliance with North American building specifications for granite dimension stone regarding density, water absorption, and compressive limits.
Reinforced Sea-Crate Packaging
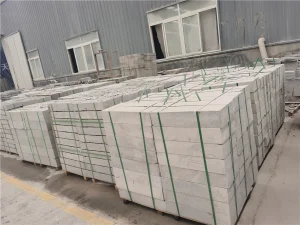
Heavy-duty, ISPM-15 compliant fumigated wooden crates secured with plastic-wrapped corner protectors, internal foam dividers, and steel banding to withstand severe container movement during sea freight.
Frequently Asked Questions (FAQ)
Expert insights from our senior quarry directors and stone application engineers.
What makes China Moonlight White Granite superior to other white granites like G603 or G602?
How do manufacturers handle shade and grain consistency for large-scale projects (>50,000 m²)?
What is the recommended surface finish for exterior plaza paving in freezing climates?
Can China Moonlight White Granite be customized for kerbstones, radial arches, and carved elements?
What lead times and container loading capacities can buyers expect for international export orders?
Does white granite require surface sealing or anti-staining chemical treatments?
Complete Dimensional Stone & System Portfolio
Discover our broader spectrum of white, grey, red, green, and specialized building facade products.
Partner with China's Premier White Granite Quarry Manufacturer
Request physical stone sample boxes, complete petrographic lab test certifications, or project estimating assistance from our engineering team in Rizhao, Shandong.
