Direct Quarry Stock · Batch Verified
Engineered Natural Granite Catalog — Core Architectural Lines
Directly sourced structural blocks, gang-saw calibrated slabs, and precision-cut architectural tiles processed under stringent dimensional tolerances.
China G3401 Shanxi Black Granite Manufacturer, Factory
View Specifications
Wholesale G654 Sesame Black Granite Polished Slabs Suppliers, Factories
View Specifications
China G614 Sesame Grey Granite Slabs & Tiles Supplier, Suppliers
View Specifications
Wholesale G386 Shidiao Red Granite Tiles Manufacturers, Suppliers
View Specifications
Wholesale Chinese Culture Granite: Stone Chronicles a Millennium
View Specifications
Wholesale G602 Sesame White Granite Manufacturer, Supplier
View Specifications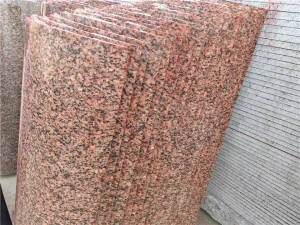
Wholesale G352 General Red Granite Cladding Panels Manufacturers
View Specifications
Industry Intelligence & Material Science
Market Dynamics of Black and Copper Granitic Lithology
High-iron, feldspathic mineral veins blended into crystalline anorthosite and gabbro matrix provide an unmatched aesthetic balance of biophilic warmth and deep metamorphic density.
Shifting Demographics in Modern Architecture
Architects worldwide are pivoting from monochromatic cold stones toward materials presenting dynamic optical warmth. Black and copper granite features naturally occurring biotite, bornite, and oxidized orthoclase feldspar that provide copper-golden flecks embedded in an impenetrable black carboniferous mantle. This responds directly to the growing demand for corporate facades that shimmer under varying solar angles while maintaining rigid structural integrity.
Geological Rarity & Block Yield Efficiency
Unlike standard homogenous grey granites, copper-veined black deposits require laser-guided diamond wire sawing at the quarry face to preserve continuous tectonic veining. Advanced geophysical ultrasound imaging enables our extraction engineers to harvest Grade-A raw blocks with volumetric integrity exceeding 94%, ensuring minimal internal fissures and ensuring predictable color uniformity across thousands of square meters.
Thermal & Chemical Resistance Advantage
Compared to engineered quartz or composite resin panels that suffer UV resin degradation and thermal shock breakdown, authentic plutonic granite offers an innate melting point above 1,200°C. Its negligible coefficient of thermal expansion makes black and copper granite exceptionally resilient against freeze-thaw spalling, exterior curtain wall expansion stress, and abrasive chemical weathering in dense urban centers.
Enterprise Procurement Strategy
Meeting Institutional Supply Chain Mandates
International EPC contractors, commercial developers, and procurement conglomerates evaluate natural stone producers on systemic reliability rather than unit price alone.
150,000+
m² Annual Capacity
±0.5mm
Thickness Calibrated
0.12%
Water Absorption
100%
Dry-Lay Verified
Tier-1 Batch Consistency
The primary hazard in large-format commercial contracts is visual disunity caused by vein variance across multiple quarry benches. Our Rizhao Haichen processing hubs enforce algorithmic color-spectrometry sorting. Slabs are categorized into tight chromo-bands, guaranteeing that multi-phase airport or campus developments retain identical optical depth.
Zero-Lag Lead Times
Disrupted supply chains stall skyscraper envelope completions. Operating directly adjacent to primary extraction reserves and within minutes of Rizhao Port and Qingdao Maritime Terminal, our logistics infrastructure bypasses standard freight chokepoints, executing prompt inland port transfers and rapid container manifest sign-offs.
BIM & Parametric Integration
Modern engineering contracts require detailed 3D digital asset libraries. Haichen provides Revit-ready parametric BIM families alongside photometric texture maps (diffuse, normal, roughness, displacement) for all our black, copper, and composite granite offerings, streamlining architect approvals during schematic design.
Comprehensive ESG Provenance
Enterprise stakeholders require verifiable carbon metrics. Our natural stone extraction processes run on closed-loop slurry recycling and electrified overhead gantry systems, achieving an embodied carbon footprint significantly lower than glazed ceramic facades, terracotta, or manufactured solid quartz surfaces.
Empirical Data & Testing Protocols
Engineered Physical & Mechanical Performance Benchmarks
Every production batch undergoes exhaustive laboratory auditing compliant with ASTM C615, EN 1341, and ISO 9001:2015 stone cladding criteria.
| Physical / Mechanical Property | Standard Test Method | ASTM Standard Requirement | Haichen Black & Copper Range | Engineering Implications |
|---|---|---|---|---|
| True Density (Apparent) | ASTM C97 / EN 1936 | ≥ 2,560 kg/m³ | 2,980 – 3,050 kg/m³ | Ultra-dense crystalline structure resists deep micro-pore weathering. |
| Water Absorption by Weight | ASTM C97 / EN 13755 | ≤ 0.40 % | 0.09 – 0.14 % | Practically impervious; eliminates freeze-thaw sub-surface hydraulic spalling. |
| Compressive Strength (Dry) | ASTM C170 / EN 1926 | ≥ 131 MPa | 210 – 235 MPa | Ideal for high-load civic plazas, heavy vehicular curbs, and multi-tier plinths. |
| Flexural Strength (Modulus of Rupture) | ASTM C99 / ASTM C880 | ≥ 10.3 MPa | 16.8 – 21.2 MPa | Allows thinner ventilated curtain wall paneling without anchoring blowouts. |
| Abrasion Resistance (Ha) | ASTM C241 / EN 14157 | ≥ 25 Ha | 62 – 78 Ha | High quartz & pyroxene ratio prevents traffic scuffing in international transit hubs. |
| Thermal Shock Resistance | EN 14066 | Pass 20 Cycles | Pass 50+ Cycles (No Fissures) | Stable under intense temperature extremes from Nordic winters to Gulf heat. |
Need Batch-Specific Certified Lab Analysis?
We supply full third-party test reports (SGS, TUV, Bureau Veritas) and comprehensive factory inspection dossiers with dry-lay serial photography for every commercial export container.
Compliance, QA & Risk Mitigation
Worldwide Export Assurance & Site-Ready Logistics
From digital slab shop drawings to seaport customs clearance, our end-to-end framework mitigates the financial risks of cross-border procurement.
Full Factory Pre-Assembly (Dry-Lay)
For complex architectural elevations, curved stone features, and expansive plaza lobbies, we perform dry-lay pre-assembly in our Rizhao facility. Slabs are arranged, photo-documented from elevated gantries, and numerically labeled. This ensures seamless on-site contractor installation with zero ambiguity regarding grain alignment.
ISPM-15 Export Packaging
Maritime transport requires specialized crate engineering. We utilize reinforced, IPPC-certified fumigated hardwood frames, complete with interior waterproof vapor barriers, shock-absorbing corner braces, and high-tensile steel strapping. Slabs are cushioned with high-density EVA foam sheets to prevent micro-chatter edge chipping.
Multilingual Technical Support
Our dedicated international stone trade engineering unit provides rapid-response coordination across English, Chinese, French, and Spanish time zones. We assist specifiers with wind-load engineering calculations, anchoring system compatibilities, sub-frame load profiles, and tailored maintenance schedules.
Technology Roadmap
The Next Decade of Stone Manufacturing Intelligence
Deploying Industry 4.0 automation to transition natural stone processing from heavy artisanal craft into an exact, low-emission architectural science.
Phase 01 · Present
AI Spectrometry Optical Sorting
Real-time slab surface scanning calibrates color saturation, bornite concentration, and mica pattern uniformity, minimizing post-shipment color variations.
Phase 02 · 2026-2027
Ultra-Thin Honeycomb Backing
Automated polyurethane epoxy bonding of 6mm natural granite skins to aerospace aluminum honeycomb, reducing dead load on exterior curtain walls by up to 65%.
Phase 03 · 2027-2028
Zero-Discharge Circular Slurry
100% recycling of stone processing slurry into compressed eco-aggregates and permeable pavers, eliminating industrial landfill overhead entirely.
Phase 04 · 2028+
Autonomous 5-Axis CNC Profiling
Direct CAD/CAM toolpath carving without human intervention, producing fluid parametric monoliths and compound-curved facades at high repeatable precision.
Procurement & Technical Queries
Frequently Asked Questions for Project Specifiers
Clear technical clarification for commercial purchasers, façade engineers, and global stone distributors.
What differentiates authentic Black and Copper granite from treated black stones?
Authentic black and copper granite features naturally occurring copper-toned orthoclase feldspar and bornite minerals crystallized directly inside anorthosite/gabbro formations over millions of years. Lower-grade processors occasionally dye porous grey granite with carbon pigments or epoxy dyes to imitate black stones. Such treatments rapidly fade, peel, and chalk when exposed to sunlight and rain. Haichen exports strictly 100% natural, untreated, geologically tested plutonic stones with verifiable thermal stability.
How do you ensure thickness and size tolerances for high-rise ventilated facades?
We use multi-head automatic bridge calibrating lines that machine every slab to an exact tolerance of ±0.5 mm in thickness, and computerized five-axis bridge saw cutting with diagonal tolerance within ±0.5 mm. Slabs calibrated to these standards eliminate irregular offsets, prevent joint unevenness, and maintain uniform anchor-pin loading across curtain wall frameworks.
Which surface finishes are recommended for freeze-thaw exterior pedestrian environments?
Flamed (thermal), bush-hammered, or water-jet textured finishes are specifically engineered for exterior flatwork and pedestrian walkways. These finishes expose the granitic quartz matrix, producing a durable microscopic profile with wet pendulum slip resistance test ratings exceeding PTV ≥ 45 (R11 or R12 equivalent), significantly exceeding ADA slip-resistance requirements even during heavy rain or freezing conditions.
What is your minimum order quantity (MOQ) and production cycle time?
Our standard commercial MOQ is one 20-foot full container load (FCL), which equates to approximately 400 to 550 m² of 20 mm slabs (or ~300 m² of 30 mm pavers), calibrated to container maritime weight thresholds (21 to 27 metric tons depending on the destination port regulations). Standard production lead time is 15 to 25 days following shop drawing confirmation and sample approval.
Can Haichen Stone provide complementary building systems and metals?
Yes. Beyond quarried slabs, pavers, kerbstones, and complex carved architectural profiles, our integrated Rizhao manufacturing cluster fabricates stainless steel glass clamp systems, structural steel sub-frames, and thermally broken commercial doors and windows. This allows major contractors to consolidate structural packages, simplify customs manifests, and significantly reduce logistics overhead.
How are container loads insured against micro-cracking and transit shocks?
Beyond solid fumigated A-frame timber crating, each maritime container is secured using high-tensile polyester cargo lashings, dynamic pneumatic air-bags, and specialized center-of-gravity stabilization chocks. Every shipment includes comprehensive Marine Cargo Insurance (All Risks ICC A) protecting your investment from factory gate loading until arrival on site.
Comprehensive Factory Selection
Specialty Natural Stone & Granite Cladding Series
Precision-manufactured kerbstones, custom landscape elements, and distinctive regional granites calibrated for immediate global deployment.
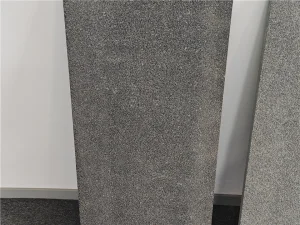
Wholesale G684 Fuding Black Granite Factories, Factory
View Specifications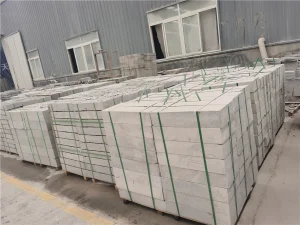
Wholesale Limestone Granite: Nature's Dual Gift Manufacturer
View Specifications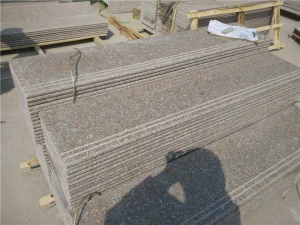
Wholesale G368 Wulian Red Granite Paving Stones Supplier
View Specifications
China A1684 Golden Hemp Granite Countertops Manufacturer
View Specifications
China G3701 Binzhou Blue Granite Suppliers, Factory
View Specifications
China Other Colours Granite – Custom Orders Manufacturers
View Specifications
Wholesale G3760 Shandong White Marble Granite Manufacturers
View Specifications