
Engineered Natural Stone & Commercial Granite Collections
Precision-calibrated stone modules manufactured in strict compliance with international engineering tolerances. Directly sourced from factory lines for large-scale hospitality, municipal, and architectural developments.
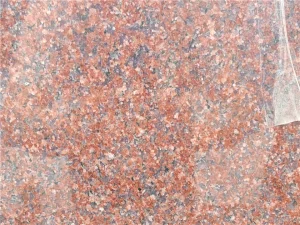
Wholesale G386 Shidiao Red Granite Tiles Manufacturers, Suppliers
View Product Specs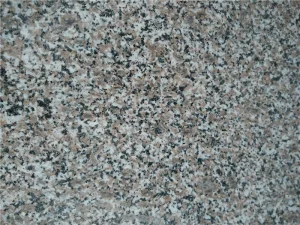
China Other Colours Granite – Custom Orders Manufacturers, Factories
View Product Specs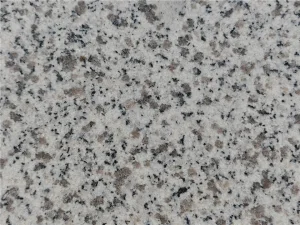
Wholesale G3760 Shandong White Marble Granite Manufacturers, Suppliers
View Product Specs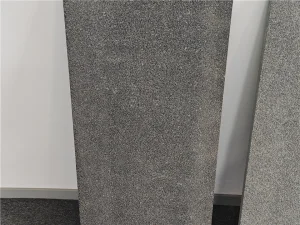
Wholesale G684 Fuding Black Granite Factories, Factory
View Product Specs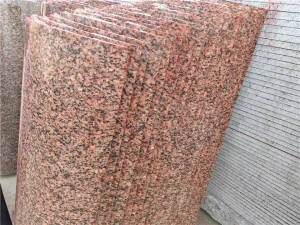
Wholesale G352 General Red Granite Cladding Panels Manufacturers, Factories
View Product Specs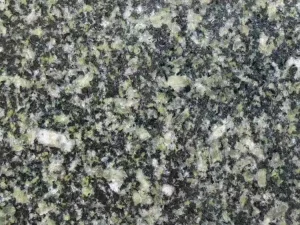
China G4101 Forest Green Granite Veneer Panels Supplier, Factories
View Product Specs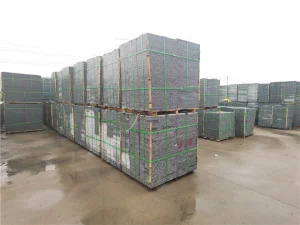
China G3702 Snowflake Blue Granite Manufacturers, Supplier
View Product Specs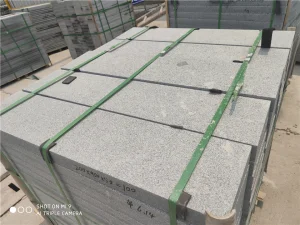
China G654 Sesame Grey Granite Flamed Finish Supplier, Factories
View Product SpecsWholesale Calacatta Borghini Marble & Ultra-Luxury Engineering
Calacatta Borghini remains one of the world's most coveted natural stones, originating exclusively from the Apuan Alps quarry basins near Carrara, Italy. In enterprise-grade procurement, industrial buyers face immense supply volatility, pricing divergence, and structural yield challenges. Modern manufacturing facilities bridge Italian raw material extraction with cutting-edge robotic dry-lay fabrication, resin reinforcement, and turnkey logistical delivery.
Quarry Yield Optimization & Block Sourcing
Calacatta Borghini is characterized by its signature warm creamy-white ground tone intersected by bold, broad grey veining accented with rare honey-gold undertones. Less than 8% of excavated blocks meet First Choice (Extra) architectural specifications. Through high-frequency acoustic flaw scanning, our engineering factories grade block soundness before sawing, mitigating intra-slab fissures and micro-fractures common in brecciated limestone formations.
Automated Gangsaw & Resin Line Integration
Slicing Calacatta Borghini requires variable-speed multi-wire saws calibrated with synthetic diamond beads to eliminate diamond wire wander. Slabs are processed through thermal degassing tunnels and infused under vacuum with UV-stable epoxy resins. Reinforced with aerospace-grade fiber mesh backing, each 20mm or 30mm slab gains high flexural strength (ASTM C880 ≥ 9.8 MPa) without yellowing over multi-decade indoor cycles.
BIM-Enabled Photogrammetric Book-Matching
Vein continuity defines the visual appraisal of Calacatta Borghini installations. High-resolution orthophotography captures every slab's coordinates to create a virtual 3D mock-up (Digital Dry-Lay). Architects and developers review complex book-matched (A/B/C/D) layouts across feature walls and islands prior to CNC bridge sawing and mitering, reducing site discard rates to under 1.2%.
Calacatta Borghini Marble & Hard Stone Comparative Spec
Architectural specifications demand transparent mechanical data. Calacatta Borghini exhibits classic recrystallized calcite structures, which behave distinctly compared to siliceous granite formations such as G603, G3760, and G654. Sourcing contracts must clearly designate the correct finishing technique to optimize abrasion resistance and stain resistance.
| Material Designation | Geological Composition | Apparent Density (kg/m³) | Water Absorption (%) | Compressive Strength (MPa) | Recommended Finishes |
|---|---|---|---|---|---|
| Calacatta Borghini | Metamorphic Calcite (≥ 98% CaCO₃) | 2,680 – 2,720 (ASTM C97) | 0.12 – 0.18 (ASTM C97) | 115 – 130 (ASTM C170) | Polished, Honed, Velvet-Leathered |
| G3760 Shandong White | Fine-Grain White Granite / Marble Alloy | ≥ 2,620 | ≤ 0.35 | ≥ 135 | Polished, Honed, Flamed |
| G603 Sesame White | Biotite Granite (Quartz-Feldspar) | 2,650 | 0.28 | 156 | Flamed, Bush-Hammered, Sawn |
| G684 Fuding Black | Basaltic / Igneous Microcrystalline | 2,950 | 0.15 | 180 | Polished, Flamed, Water-Jet |
| G654 Sesame Grey | Diorite / Fine Quartz Gneiss | 2,710 | 0.22 | 165 | Flamed, Bush-Hammered, Honed |
Localized Support, ASTM/EN Compliance, & Global Clearance
Wholesale procurement of high-value natural stone requires full documentation across customs clearing, load testing, and chemical sealing compatibility. We implement comprehensive supply protocols that protect commercial contractors from import penalties, transit damage, and technical non-compliance.
CE Certification & ASTM C503/C615 Audits
Every batch of exported stone is accompanied by certified factory test reports covering bulk density, flexural breaking load, slip resistance (DIN 51130 R9-R11), and frost-thaw durability under EN 12371. Material testing protocols align precisely with the standards mandated by North American and European structural engineers.
ISPM-15 Fumigation & Port Integration
Factory proximity to Rizhao Port and Qingdao Port gives our export shipments direct ocean freight routing. All solid-wood packaging strictly complies with ISPM-15 heat treatment and fumigation mandates. A-frame steel shipping racks are utilized for large Calacatta Borghini slabs to eliminate flexing during dynamic maritime voyages.
Hydrophobic Sealing & Anti-Efflorescence
Given the natural porous micro-channels in high-calcium marble, slabs are treated with fluoropolymer-based nano-penetrating sealers prior to boxing. This prevents moisture transmission, oil absorption, and alkaline efflorescence during mortar-bed installation, satisfying demanding Class-A LEED commercial standards.
The Future of Calacatta Borghini Fabrication: 2026–2030
As quarries reach deeper geological strata, global factories must innovate to maintain architectural feasibility and lower environmental impact. Advanced precision tooling and composite substrate engineering are transforming raw block utilization into sustainable building solutions.
Ultra-Thin 5mm Lightweight Honeycomb Panels
Through micro-blade slicing and aeronautical aluminum honeycomb lamination, Calacatta Borghini weight is reduced from 55 kg/m² to under 14 kg/m². This enables book-matched luxury marble facades in seismic zones, supertall elevator cabs, and mega-yacht interiors where static load capacity is restricted.
Zero-Sludge Closed-Loop Water Recycling
Modern sustainability standards require natural stone factories to eliminate slurry pollution. Next-generation multi-stage flocculation filter presses extract 98.5% of process water for direct workshop recycling, while compressed calcium carbonate cakes are repurposed for eco-cements and road-base aggregate.
AI Robotic Seam Matching & Micro-Chamfering
By 2027, optical vision algorithms integrated into 5-axis CNC waterjet gantries will dynamically calculate stone grain continuity at mitered returns. This produces seamless 90-degree waterfall edges on vanity tops and kitchen islands with hairline joints under 0.2mm, virtually invisible to the eye.
Heavy-Duty Granite Slabs, Curbstones & Structural Veneers
Supplying turnkey natural stone solutions from our primary quarry lines. Engineered for massive foot-traffic plazas, curtain walls, and municipal streetscapes.
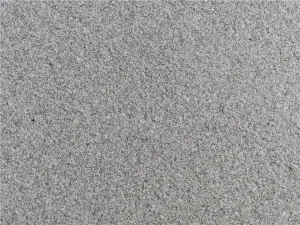
China G614 Sesame Grey Granite Slabs & Tiles Supplier, Suppliers
View Product Specs
China G3401 Shanxi Black Granite Manufacturer, Factory
View Product Specs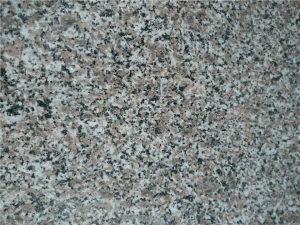
China G6361 Wulianhua Granite for Landscaping Manufacturer, Factories
View Product Specs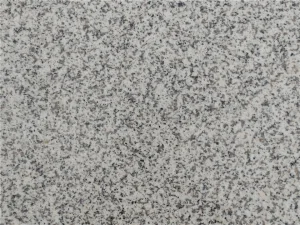
China G603 Sesame White Granite Suppliers, Factory
View Product Specs
Wholesale G654 Sesame Black Granite Polished Slabs Suppliers, Factories
View Product Specs
China A1684 Golden Hemp Granite Countertops Manufacturer, Factories
View Product Specs
China Premium Chinese Red Granite Blocks Supplier, Suppliers
View Product Specs
China G3743 Lu Grey Granite Building Stone Manufacturer, Factories
View Product SpecsWholesale Procurement & Calacatta Borghini Marble FAQ
Clear, engineer-verified answers to common technical, logistics, and material grading inquiries raised by global developers, specification writers, and stone importers.
