
Primary Red & Commercial Granite Selections
Quarry-direct dimension stone slabs, veneer panels, and engineered blocks prepared for international structural deployment.
China G4101 Forest Green Granite Veneer Panels Supplier, Factories
View Product Details
China G3702 Snowflake Blue Granite Manufacturers, Supplier
View Product Details
China Premium Chinese Red Granite Blocks Supplier, Suppliers
View Product Details
Wholesale G602 Sesame White Granite Manufacturer, Supplier
View Product Details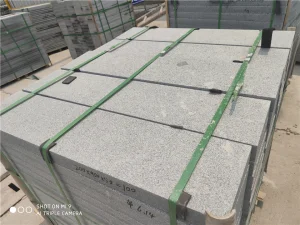
China G654 Sesame Grey Granite Flamed Finish Supplier, Factories
View Product Details
China G3701 Binzhou Blue Granite Suppliers, Factory
View Product Details
Wholesale G684 Fuding Black Granite Factories, Factory
View Product Details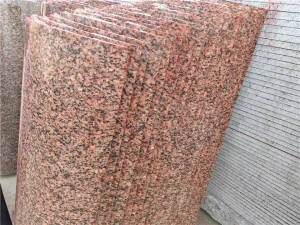
Wholesale G352 General Red Granite Cladding Panels Manufacturers, Factories
View Product DetailsRed and White Granite Solutions for Global Infrastructure
Analyzing petrological characteristics, structural resilience, and commercial supply chain dynamics for high-capacity architectural projects.
Petrological Mineral Composition
Red granite derives its rich chromatic intensity from high concentrations of alkali potassium feldspar (orthoclase), while white granite exhibits a dense matrix dominated by quartz and plagioclase feldspar. This precise mineralogical balance dictates non-porous performance and extreme flexural strength under severe environmental stresses.
Commercial Real Estate Engineering
Modern skyscraper facades and municipal superstructures utilize cut-to-size red and white granite cladding due to its thermal resistance, minimal thermal expansion coefficient, and immunity to acid rain degradation. Bulk quarry sourcing ensures aesthetic uniformities across multi-stage building developments.
High-Traffic Civil Infrastructure
Subway terminals, international airport concourses, and expansive public plazas mandate stone with an exceptional Mohs hardness (6-7). White granite varieties offer elevated light reflectance values (LRV) reducing urban heat island effects, while red granites provide high-contrast spatial zoning for pedestrian flows.
Advanced Automated Processing & Finishing Systems
From raw block extraction to precision CNC calibration: How factory integration maintains microscopic tolerances.
Diamond Wire Saw Block Extraction
Utilizing high-tensile diamond wire sawing machines in raw quarry beds eliminates micro-fracturing within red and white granite reserves. This preserves block integrity, yielding optimal yield ratios for large-format gang saw slab production.
5-Axis CNC & Waterjet Milling
Automated multi-axis CNC routers process custom radial curbing, column cladding, and intricate architectural motifs. Waterjet cutting systems deliver precise joint tolerances of ±0.5mm for high-density geometric mosaic installations.
Multi-Stage Surface Finish Technologies
Custom surface treatments alter both slip resistance (CoF) and visual tone. Automated continuous polishing lines produce mirror finishes, while high-pressure waterjet profiling and flamed treatments enhance tactile slip protection for exterior applications.
| Surface Finish | Processing Technique | Slip Resistance (CoF) | Primary Application |
|---|---|---|---|
| Polished Finish | Multi-head abrasive grinding up to 3000 grit | Dry: 0.70 | Wet: 0.35 | Interior flooring, luxury wall cladding, vanity tops |
| Flamed (Thermal) | High-temperature oxy-acetylene torch thermal shock | Dry: 0.85 | Wet: 0.75 | Outdoor plazas, walkways, municipal steps |
| Bush-Hammered | Hydraulic multi-point carbide head impact | Dry: 0.90 | Wet: 0.80 | Heavy pedestrian zones, landscaping, kerbstones |
| Honed Finish | Smooth mechanical satin grinding to 400 grit | Dry: 0.65 | Wet: 0.50 | Commercial interior lobbies, high-traffic corridors |
| Leathered / Brushed | Diamond-impregnated filament brush burnishing | Dry: 0.75 | Wet: 0.60 | Textured feature walls, executive countertops |
Localized Application Scenarios for Red & White Granite
Specific architectural deployment cases optimized for climatic durability, load-bearing capability, and aesthetic permanence.
Anchored Rainscreen Cladding
Engineered red and white granite slabs (minimum 30mm thickness) integrated into stainless steel dry-hanging facade systems. This design creates a pressure-equalized drainage cavity that prevents moisture ingress, protects thermal insulation, and withstands typhoon-grade wind loads.
Urban Transit & Civic Hardscaping
Flamed sesame white and general red granite paving stones (60mm to 100mm thickness) designed for heavy vehicular loading. Used extensively in transit hubs, bus rapid transit (BRT) lanes, and municipal sidewalks, providing long-term structural integrity with minimal maintenance.
Hospitality & Luxury Interiors
Polished Chinese Red and Shandong White granite utilized for grand atrium flooring, reception counters, and interior accent walls. The material's natural resistance to staining, chemical degradation, and surface scratching makes it superior to softer engineered marbles.
International Standards Compliance & Freight Protection
Comprehensive export protocols ensuring full compliance with European CE standards, ASTM specifications, and international maritime logistics.
Rigorous ASTM & EN Standard Testing
All wholesale granite shipments are verified through independent laboratory testing under ASTM C615 (Standard Specification for Granite Dimension Stone) and EN 1341/1343. Factory certificates document compressive strength, flexural resistance, density, and freeze-thaw endurance cycle compliance.
Dry-Lay Inspections & Color Matching
To eliminate chromatic variance in large cladding projects, our factory conducts full-scale pre-shipment dry-lay assemblies. Slabs are color-sorted under natural light conditions, numbered sequentially per shop drawings, and packed to simplify on-site installation.
ISPM 15 Certified Export Packaging
Granite slabs and cut-to-size pavers are secured in heavy-duty, fumigated solid wood crates lined with polyethylene foam protection. Crates feature integrated steel banding, corner protectors, and customized A-frame racks to withstand trans-oceanic container transit.
Specialized Granite Slabs, Tiles & Architectural Elements
Explore our extensive portfolio of custom cut-to-size white, red, black, and grey granite inventory ready for containerized worldwide dispatch.
China G3401 Shanxi Black Granite Manufacturer Factory
View Product Details
Wholesale Limestone Granite: Nature's Dual Gift Manufacturer, Factory
View Product Details
China G6361 Wulianhua Granite for Landscaping Manufacturer, Factories
View Product Details
China G603 Sesame White Granite Suppliers, Factory
View Product Details
China G3743 Lu Grey Granite Building Stone Manufacturer, Factories
View Product Details
Wholesale G654 Sesame Black Granite Polished Slabs Suppliers, Factories
View Product Details
Wholesale G368 Wulian Red Granite Paving Stones Supplier, Suppliers
View Product Details
Wholesale G3760 Shandong White Marble Granite Manufacturers, Suppliers
View Product DetailsEco-Friendly Mining & Zero-Waste Stone Fabrication
Implementing circular economic practices in natural stone extraction to minimize environmental impact and maximize energy efficiency.
Closed-Loop Water Recycling
Our stone processing facilities operate continuous closed-loop filtration plants. Over 95% of industrial water used in gang sawing, wire cutting, and polishing is clarified and recirculated, eliminating wastewater discharge into local watersheds.
Stone Slurry Upcycling
By-products such as granite powder and saw slurry are compressed into dense aggregate materials used in high-grade concrete formulations, road base stabilization, and eco-friendly paving bricks, driving zero-landfill manufacturing goals.
Solar Energy Quarry Operations
Integrating roof-mounted photovoltaic solar arrays across our primary processing workshops drastically lowers the embodied carbon footprint of processed granite slabs, aligning with global green building standards (LEED / BREEAM).
Wholesale Granite Procurement FAQ
Direct technical answers for commercial project specifiers, stone importers, structural engineers, and procurement teams.
What is the standard Minimum Order Quantity (MOQ) for wholesale red and white granite orders?
Our baseline Minimum Order Quantity is typically one full 20-foot heavy-duty container (approx. 400–600 m² of 20mm thick stone or 27 metric tons payload capacity). For custom architectural projects requiring mixed finishes or varying tile sizes, we offer consolidated container packing tailored to project schedules.
How does your factory ensure chromatic uniformity across multi-thousand meter orders?
Color consistency is managed directly at the quarry level by extracting raw blocks from identical mineral veins. During factory gang-sawing, slabs are tagged in extraction sequence. We perform pre-shipment dry-lay sorting under standardized lighting to ensure smooth gradient distribution prior to crating.
What surface treatment is best suited for freezing northern climate walkways?
For climates subject to freeze-thaw cycles, we recommend flamed (thermal), bush-hammered, or waterjet-etched finishes in a minimum thickness of 30mm. These textures provide an anti-slip rating of R11-R13 while maintaining open surface pores that allow trapped subsurface moisture to escape without causing spalling.
Can your factory produce custom curved kerbs and complex 3D CNC carvings?
Yes. Our workshop is equipped with 5-axis interpolating CNC machines, automated wire saws, and 3D digital scanners. We process custom radius kerbstones, solid stone column capitals, tapered balustrades, and complex relief sculptures straight from CAD / BIM drawings.
What testing documentation do you provide for municipal structural approval?
We provide full laboratory test dossiers for every batch, including density (ASTM C97), compressive strength (ASTM C170), flexural strength (ASTM C880), thermal shock resistance, and slip resistance ratings. Third-party inspection reports (SGS, TUV, Intertek) are available upon request.
