Featured Quarry-Direct Stone Slabs & Fabricated Solutions
Explore our top verified architectural materials produced under European stone processing standards with automated sizing and precision edge finishing.
China G3702 Snowflake Blue Granite Manufacturers, Supplier
View Product Specs
China G603 Sesame White Granite Suppliers, Factory
View Product Specs
China A1684 Golden Hemp Granite Countertops Manufacturer, Factories
View Product Specs
China G6361 Wulianhua Granite for Landscaping Manufacturer, Factories
View Product Specs
China G3401 Shanxi Black Granite Manufacturer, Factory
View Product Specs
Wholesale G3760 Shandong White Marble Granite Manufacturers, Suppliers
View Product Specs
Wholesale G368 Wulian Red Granite Paving Stones Supplier, Suppliers
View Product Specs
Wholesale G602 Sesame White Granite Manufacturer, Supplier
View Product SpecsGeological Origins & Material Characteristics of St Laurent Marble
Unveiling the crystallization science, vein morphology, and petrological distinction of premium dark chocolate and golden-veined calcite stone.
St Laurent Marble (historically termed Noir Saint Laurent or Marbre Saint-Laurent) represents one of the most distinctive semi-metamorphic luxury limestones in modern architectural stone masonry. Characterized by a dense, crystalline micro-sparitic calcite matrix ranging from profound dark cocoa to obsidian black, this natural masterpiece is traversed by a dynamic poly-directional network of crystalline calcite fissures, oxidized iron strings, and burnished copper-gold veining.
From a petrographical perspective, St Laurent stone is classified under ASTM C503 (Standard Specification for Marble Dimension Stone - Exterior and Interior). Unlike conventional dolomitic stones or soft sedimentary limestones, high-grade St Laurent demonstrates exceptional density (~2,710 kg/m³) and an ultra-low effective porosity. The intricate veins are not superficial fissures; rather, they are healed tectonic recementations where interstitial mineral-rich hydro-thermal fluids introduced trace chalcopyrite, hematite, and limonite during deep-crust metamorphic recrystallization.
When selecting St Laurent marble slabs at an industrial wholesale scale, global specifiers distinguish between the classic Mediterranean extraction pockets and premium Chinese processing hubs. While European quarries yield historical provenance, China's advanced natural stone manufacturing facilities—predominantly concentrated in coastal industrial corridors such as Shandong and Fujian—have pioneered industrialized block processing, vacuum-epoxy consolidation, and ultra-flat gangsaw slicing, transforming raw blocks into structurally stabilized, bookmatched master-grade slabs at an unmatchable procurement economy.
Polychromatic Vein Morphology
Featuring distinct copper, ochre, and crystalline white calcitic veins intersecting a deep carbonaceous groundmass. Perfect for continuous bookmatching in monumental vertical wall applications.
Petrophysical Density
Compressive strength reaching up to 142 MPa with water absorption below 0.22%, meeting stringent European (EN 1469) and North American (ASTM C503) structural criteria.
Vacuum Resin Stabilization
Engineered through multi-stage oven curing and Italian automated vacuum-line resin penetration, mitigating micro-fissure expansion during overseas transit and mechanical cutting.
Chinese Factory Supply Chain Advantages: Smart Automation & Port Clustering
How Shandong and Rizhao manufacturing clusters combine high-speed diamond wire saws, Breton polishing arrays, and direct sea-freight hubs to optimize bulk procurement.
The global natural stone supply chain has evolved from localized quarrying to an integrated, planetary ecosystem. China has consolidated its dominance as the world's most sophisticated fabrication, calibration, and finishing powerhouse for premium stones, including St Laurent Marble. Choosing a specialized Chinese manufacturer like Haichen Stone offers tier-one procurement directors tangible competitive moats: direct raw-block purchasing networks, capital-intensive multi-wire saw installations, digitized dry-lay scanning, and port-side maritime logistics.
By leveraging multi-wire diamond sawing arrays, Chinese factories achieve kerf thickness reductions from 3.5mm down to 2.0mm. This precision elevates block yield by over 18%, directly lowering the per-square-meter cost passed onto commercial developers. Furthermore, computerized 24-head continuous slab-polishing lines utilize resinoid diamond abrasives, imparting an optical specular gloss rating exceeding 95 GU (Gloss Units) on St Laurent surfaces without the orange-peel aberrations typical of legacy manual processing.
Global Enterprise Procurement: Overcoming Color Variation & Lead-Time Risks
Systemic methodologies for general contractors, hospitality fit-out specialists, and stone importers to navigate batch matching and international ocean freight.
Digital AI Dry-Lay & Slab Sequencing
To prevent chaotic color mismatches across expansive hotel lobbies, our factory applies high-resolution 3D optical cameras to photograph every consecutive slab cut from the same block. A customized digital mockup renders the exact vein alignment before crating, eliminating on-site installation disputes.
ISPM-15 Engineered Packaging
St Laurent marble slabs demand heavy-duty, fumigated A-frame timber crates lined with closed-cell EPE polyethylene foam. Each slab face is protected with static plastic film to prevent sulfur leaching, acid spotting, or friction abrasions during 40-day transoceanic voyages.
Incoterm Risk Neutralization
Navigating FOB, CIF, or DDP demands strict alignment. We provide comprehensive mill test certificates (MTC), certified weighing slips, bill of lading (B/L) tracking, and third-party pre-shipment inspections (SGS/BV verified) to assure full contractual accountability.
Localization Support, CE Marking & North American ASTM Compliance
Ensuring St Laurent marble fabrications integrate seamlessly into municipal specifications, green building councils, and structural facade codes.
Procuring stone internationally introduces stringent regional regulatory requirements. A failure to comply with local structural anchoring, slip resistance, or volatile chemical emission standards can lead to catastrophic site halts. Our direct manufacturing plant structures its quality management systems to strictly satisfy Western building codes, environmental product declarations (EPD), and localized installation practices.
ASTM C503 / C97
Rigorous empirical testing for absorption, bulk specific gravity, modulus of rupture (ASTM C99), and flexural strength under compressive loads for USA & Canadian projects.
CE Certification (EN 1469)
Full Factory Production Control (FPC) accreditation compliant with European Union Construction Products Regulation (CPR 305/2011/EU) for dimension stone cladding.
LEED v4.1 Credits
100% natural, non-toxic stone emitting zero VOCs. Eligible for Material and Resources (MR) credits under regional extraction and lifecycle sustainability criteria.
DCOF & Slip Ratings
Engineered surface texturing (honed, brushed, leathered) achieves Dynamic Coefficient of Friction (≥0.42 per ANSI A326.3) for commercial public safety compliance.
St Laurent Marble Engineering & Physical Property Data Matrix
Standard laboratory reference values for architectural specification and shop drawing load calculations.
| Physical / Mechanical Property | Test Standard Method | Target Specification Metric | Typical St Laurent Factory Value | Architectural Application Suitability |
|---|---|---|---|---|
| Apparent Density (Bulk Gravity) | ASTM C97 / EN 1936 | ≥ 2,600 kg/m³ | 2,710 – 2,730 kg/m³ | High-mass feature walls, lobby cladding, vanity counters |
| Water Absorption by Weight | ASTM C97 / EN 13755 | ≤ 0.40 % | 0.18 – 0.22 % | Bathrooms, luxury thresholds, indoor water features |
| Compressive Strength | ASTM C170 / EN 1926 | ≥ 100 MPa | 135 – 145 MPa | High-traffic retail paving, stair treads, portico columns |
| Flexural Strength (Modulus of Rupture) | ASTM C99 / EN 12372 | ≥ 9.0 MPa | 12.4 – 15.1 MPa | Dry-hang curtain wall panels, cantilevered steps |
| Abrasion Resistance (Capon Test) | EN 14157 / ASTM C241 | ≤ 24.0 mm groove | 18.5 – 20.2 mm | Commercial atrium floors, luxury boutique corridors |
| Specular Gloss Rating (Polished) | ISO 2813 / ASTM D523 | ≥ 85 GU | 92 – 98 GU | Mirrored elevator vestibules, executive boardroom tables |
Localized Architectural Applications & Installation Case Scenarios
Where dramatic dark backgrounds and vibrant metallic veining deliver prestige across ultra-luxury commercial and residential environments.
Bookmatched Atrium Backdrops
In 5-star hotel lobbies and corporate headquarters, bookmatched A/B/C/D St Laurent slabs create monumental tapestry effects. Factory gangsaw indexing ensures veins flow seamlessly across 10-meter spans, framed by understated brushed brass or dark bronze reveals.
Executive Countertops & Bar Tops
With advanced factory oleophobic and hydrophobic nano-penetration sealers, St Laurent performs exquisitely as high-end restaurant bar tops, executive credenzas, and vanity consoles, resisting citrus juices, ethanol, and moisture rings.
Luxury Spa Wet Areas & Floors
Utilizing honed, leathered, or lightly waterjet-etched finishes, St Laurent achieves a tactile, velvety patina that satisfies wet-barefoot slip resistance while highlighting the undulating gold and crystalline streaks beneath architectural mood lighting.
Industry Megatrends: Composite Honeycomb Panels & Zero-Sludge Ecology
How smart manufacturers leverage lightweight aerospace honeycomb backing and circular water recycling to drive sustainable luxury construction.
The global natural stone industry is undergoing a structural transformation centered around two imperatives: structural weight reduction and ecological stewardship. Heavy 20mm and 30mm solid slabs represent significant dead loads in high-rise curtain walls, superyachts, and elevator car interiors. Leading Chinese factories have pioneered stone-honeycomb lamination technology, slicing St Laurent slabs into ultra-thin 5mm to 8mm veneers bonded directly to aircraft-grade aluminum honeycomb backing.
This composite architecture decreases dead weight by up to 70% (from ~55 kg/m² down to ≤16 kg/m²), while increasing impact flexural resistance fivefold. Furthermore, state-of-the-art Chinese stone production facilities operate closed-circuit filter-press water filtration setups. Upwards of 98% of processing water is recycled in-factory, and separated stone sludge is consolidated into high-density refractory bricks or asphalt filler, ensuring that projects sourcing from our factory align with stringent ESG and carbon-neutrality mandates.
Our 6-Tier Quality Assurance & Export Verification Protocol
A systematic breakdown of the rigorous testing protocols every slab and cut-to-size crate must pass before sea-container dispatch.
1. Ultrasonic Flaw Detection
Prior to gangsaw slicing, raw blocks undergo non-destructive ultrasonic resonance testing to detect latent internal fractures, dry cracks, and structural clay pockets, eliminating hidden fissures.
2. Laser Dimension Verification
Automated dual-axis laser calipers monitor slab thickness throughout diamond blade grinding, ensuring exact planar parallelism within an uncompromising tolerance of ±0.5mm across the slab.
3. Spectrophotometric Color Grading
Slabs are systematically grouped by background chromaticity and vein saturation using CIE L*a*b* spectrophotometers, ensuring that crates allocated to a single project zone share uniform tone values.
4. High-Gloss Optical Inspection
Surface sheen is verified using multi-angle micro-glossmeters at 60° geometry. Any slab falling below 90 GU is re-routed through fine-grit oscillating polishing heads for corrective re-finishing.
5. Physical Mockup & Dry-Lay
For high-profile hotel foyers, all bookmatched slabs are laid out horizontally in our 5,000m² dry-lay hall, labeled with alphanumeric layout codes, photographed, and approved via client video audit.
6. Solid Timber Export Crating
Heavy-gauge pine bundles are heat-treated per ISPM-15, strapped with galvanized steel tensile banding, and secured within 20ft heavy-duty containers using timber bracings and desiccant bags to prevent moisture damage.
Frequently Asked Questions (FAQ) for St Laurent Marble Sourcing
Direct technical and commercial answers for stone importers, commercial architects, and procurement teams.
Wholesale Granite, Marble & Precision Building Stone Catalog
Explore our full spectrum of specialized natural stone selections manufactured with precision tolerances for worldwide mega-infrastructure and commercial facades.
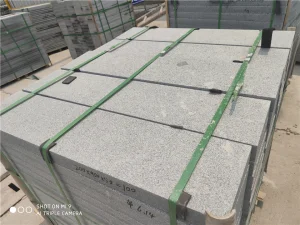
China G654 Sesame Grey Granite Flamed Finish Supplier, Factories
View Product Specs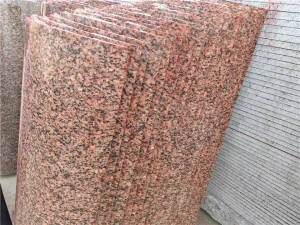
Wholesale G352 General Red Granite Cladding Panels Manufacturers, Factories
View Product Specs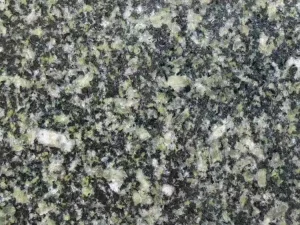
China G4101 Forest Green Granite Veneer Panels Supplier, Factories
View Product Specs
China Premium Chinese Red Granite Blocks Supplier, Suppliers
View Product Specs
Wholesale Chinese Culture Granite: Stone Chronicles a Millennium, Artistry Inherits the Orient Manufacturer, Suppliers
View Product Specs
China Other Colours Granite – Custom Orders Manufacturers, Factories
View Product Specs
Wholesale Limestone Granite: Nature's Dual Gift Manufacturer, Factory
View Product Specs